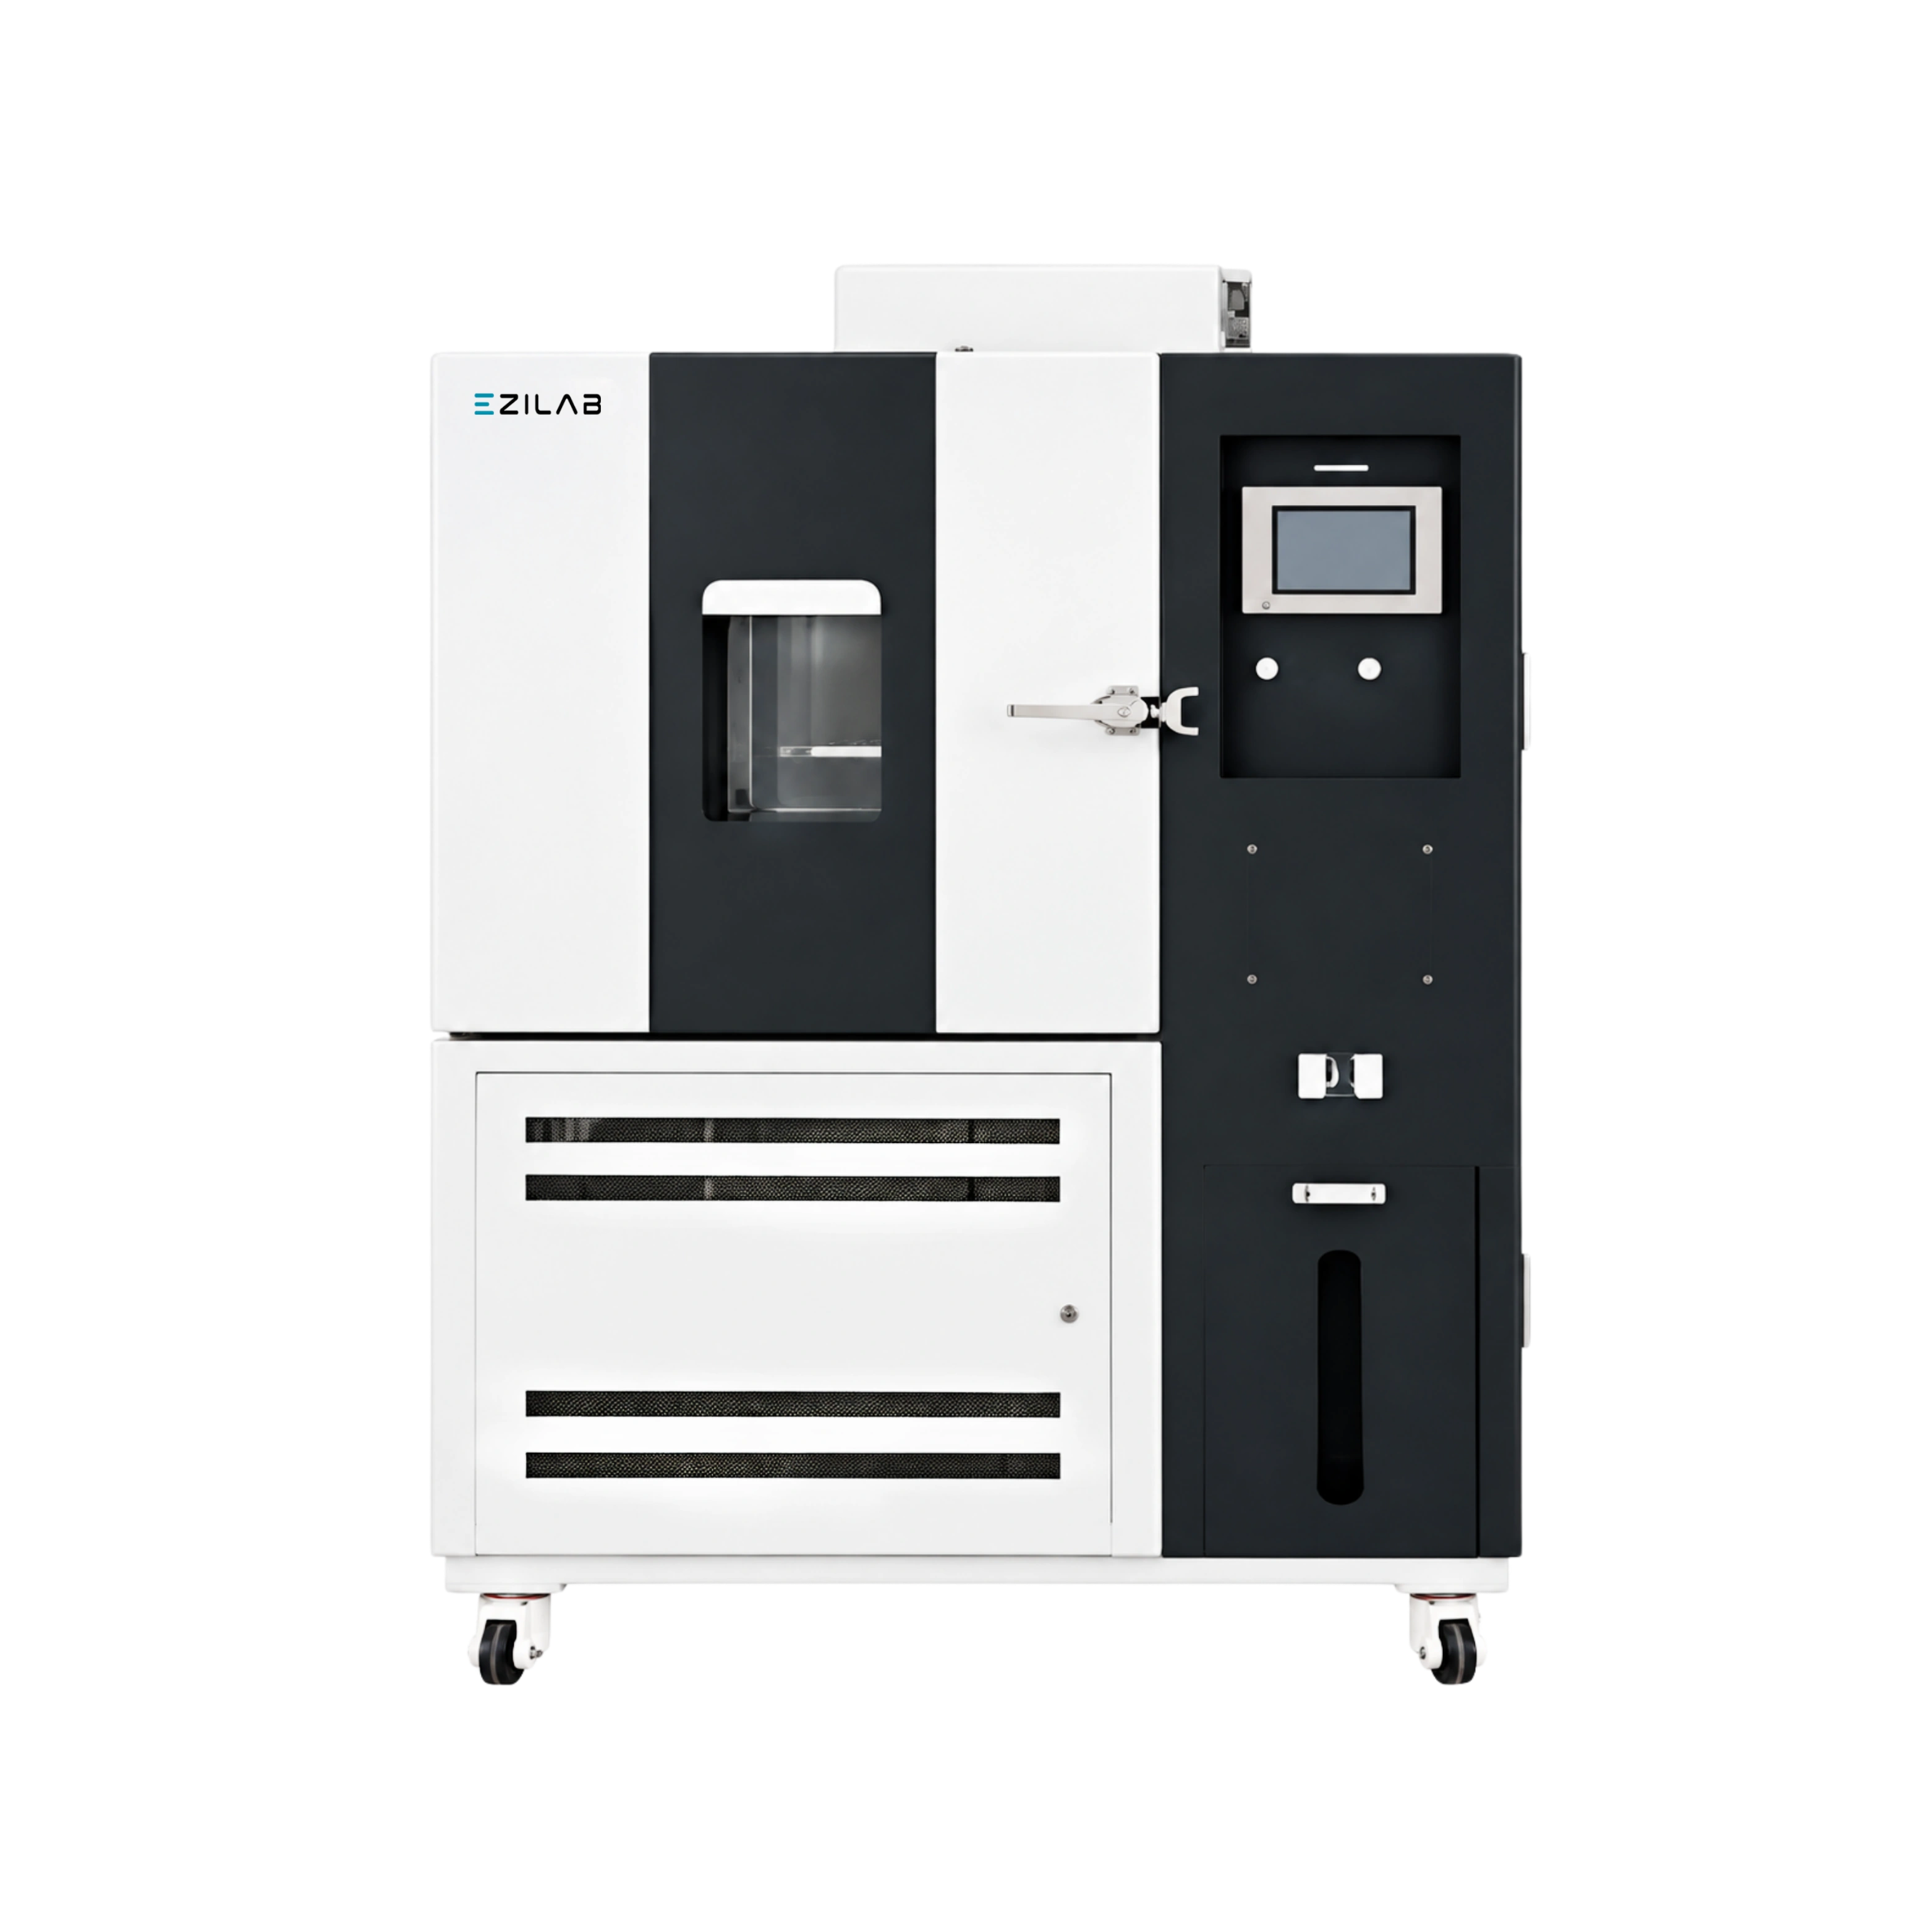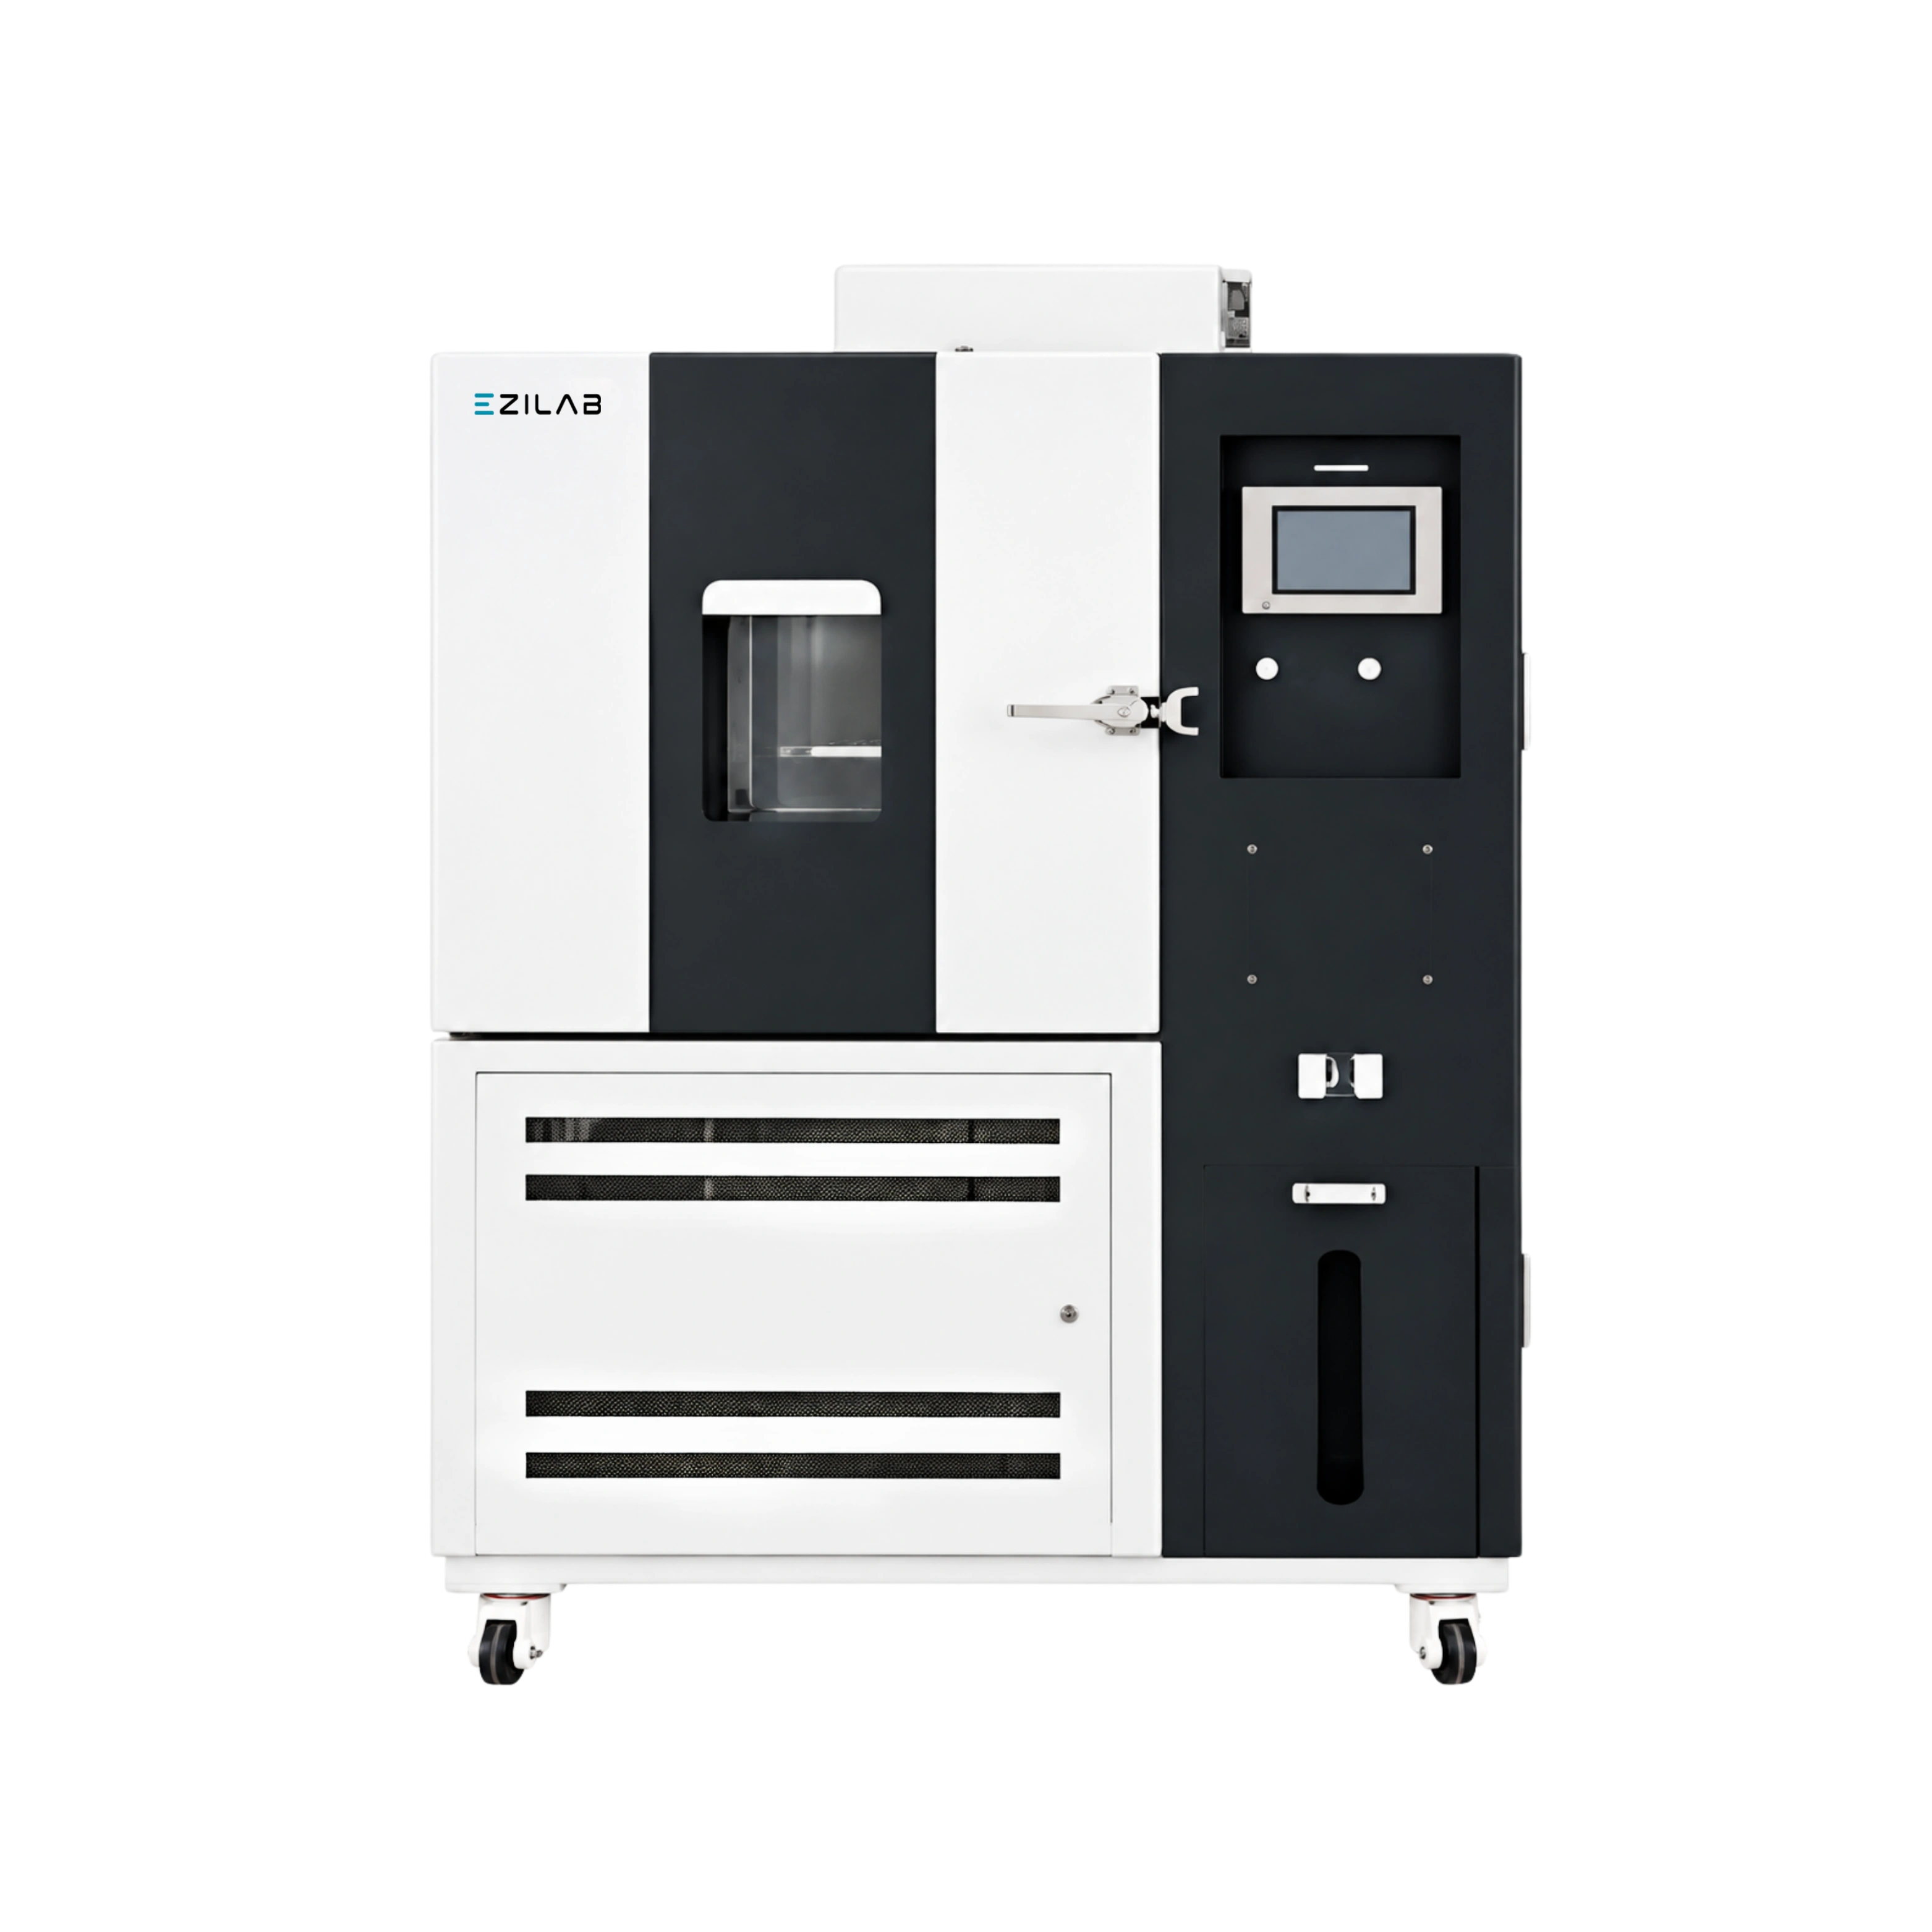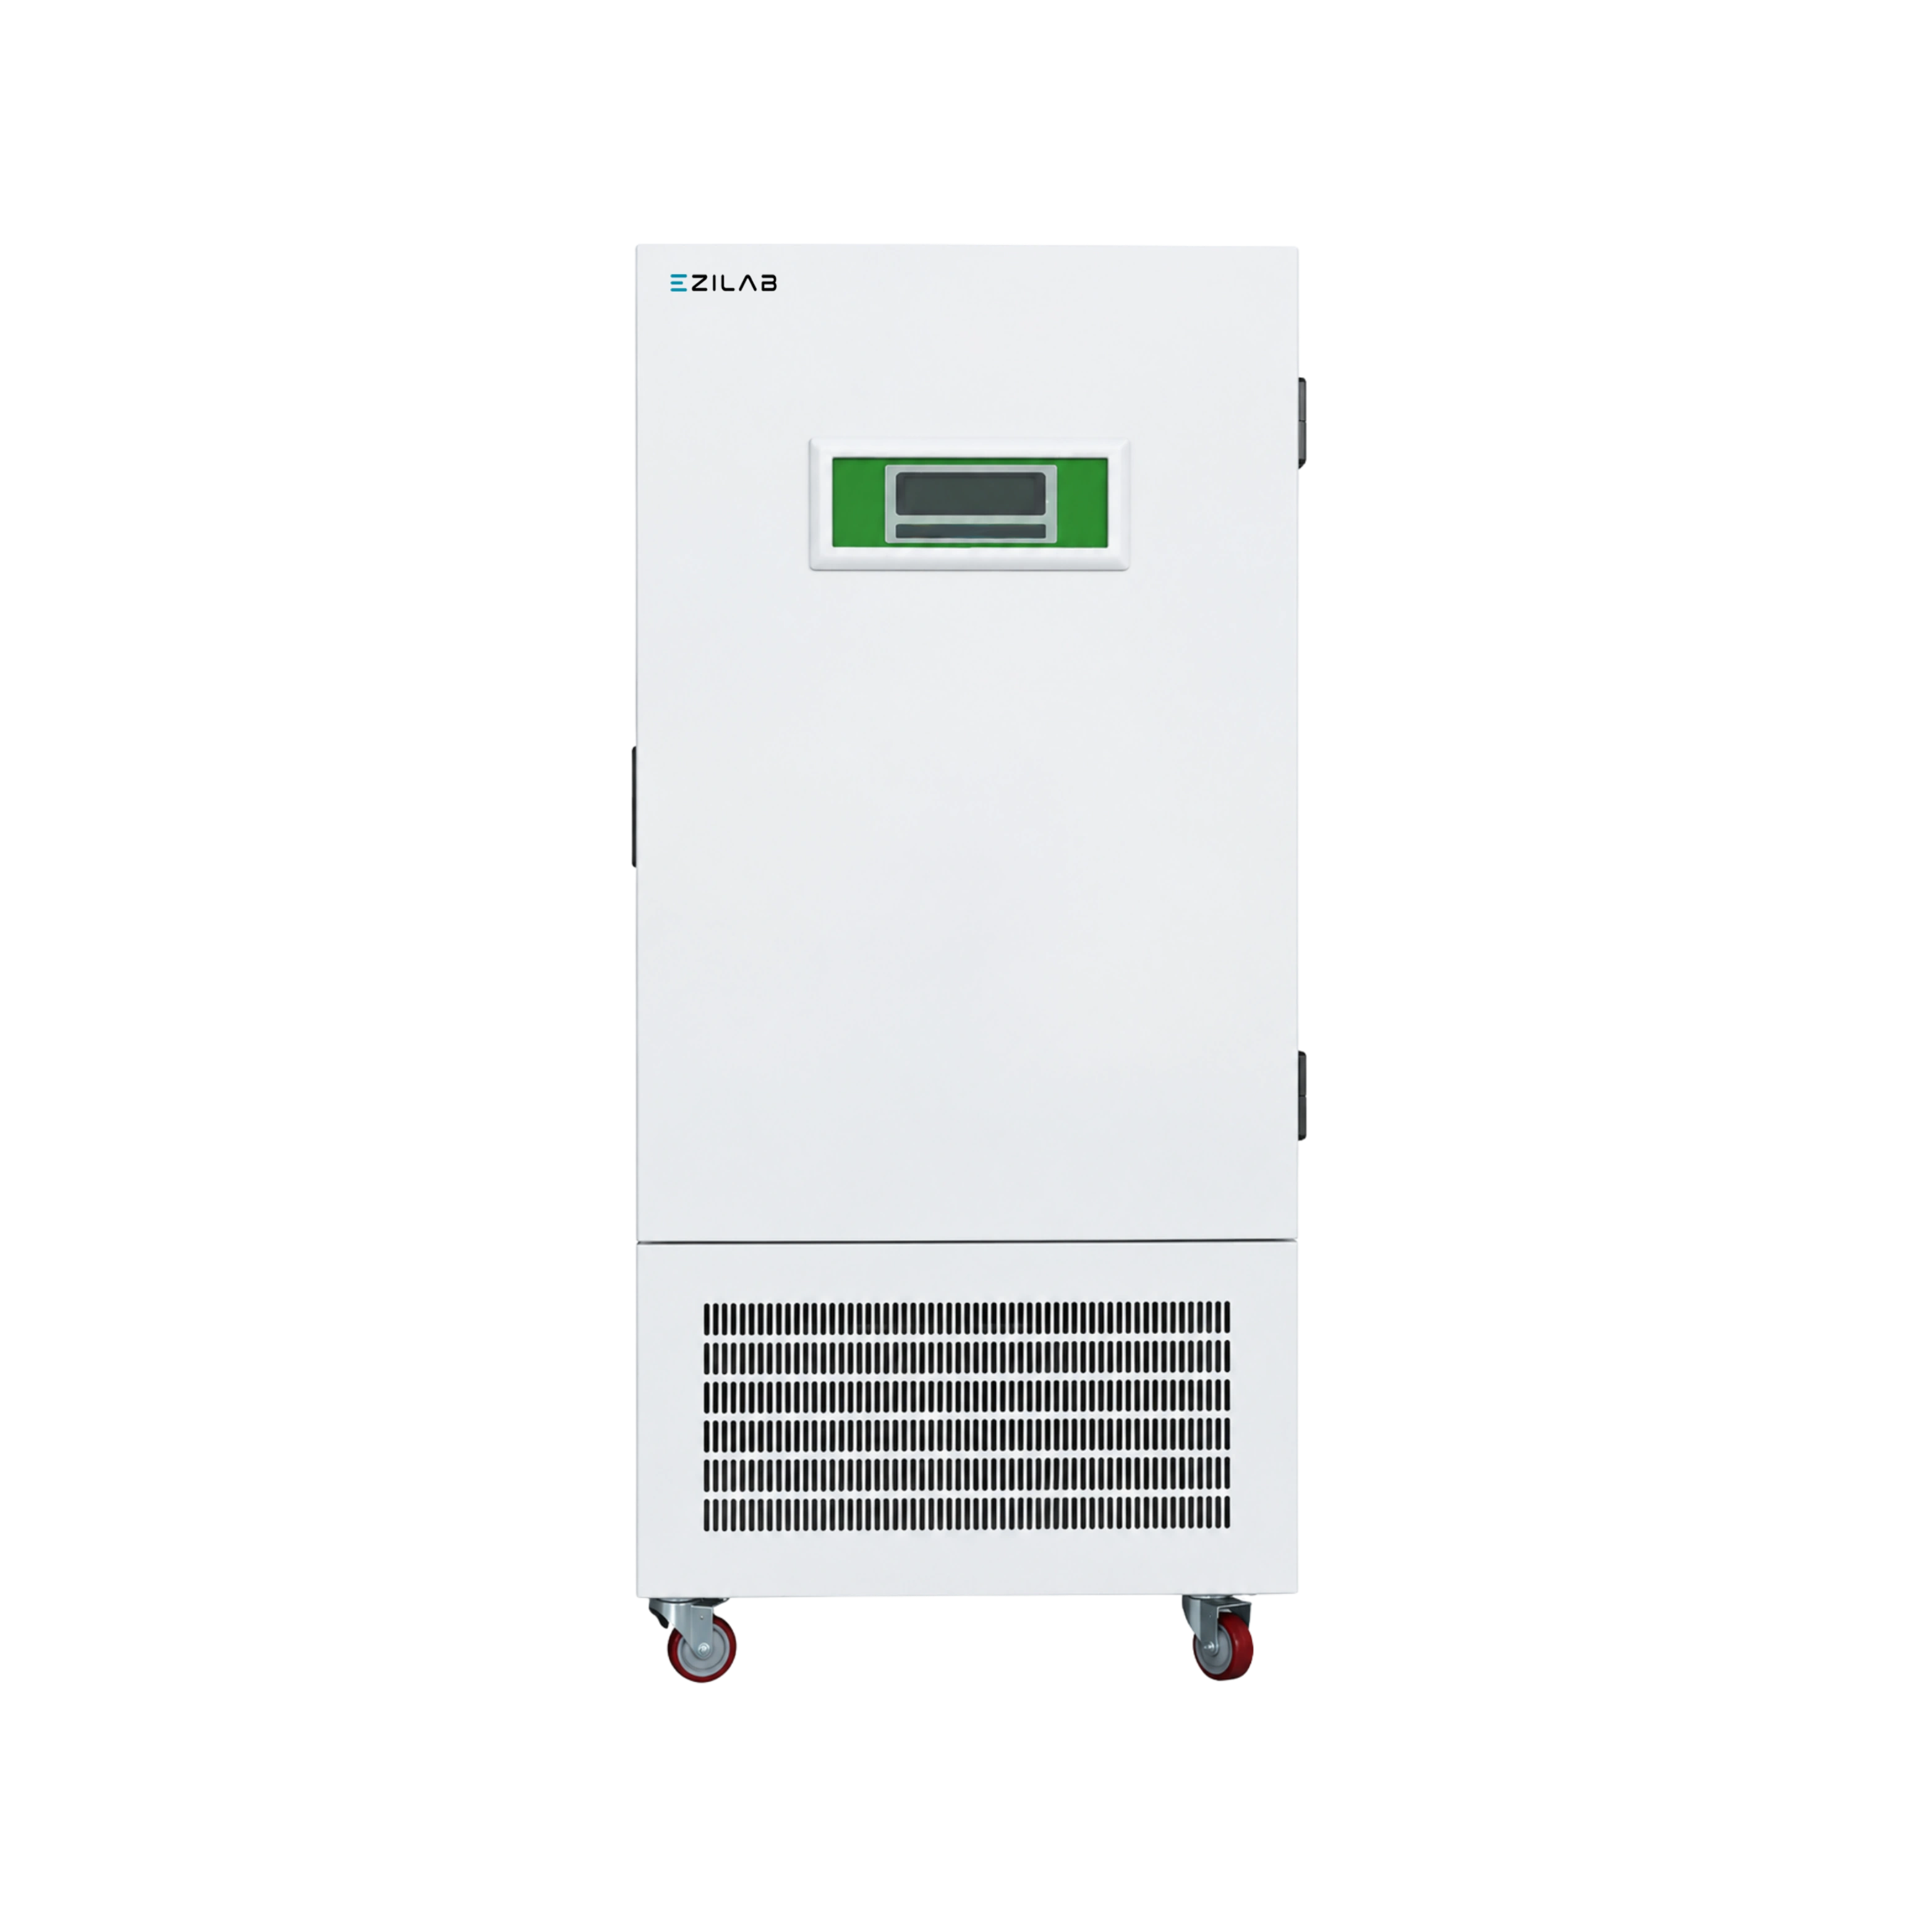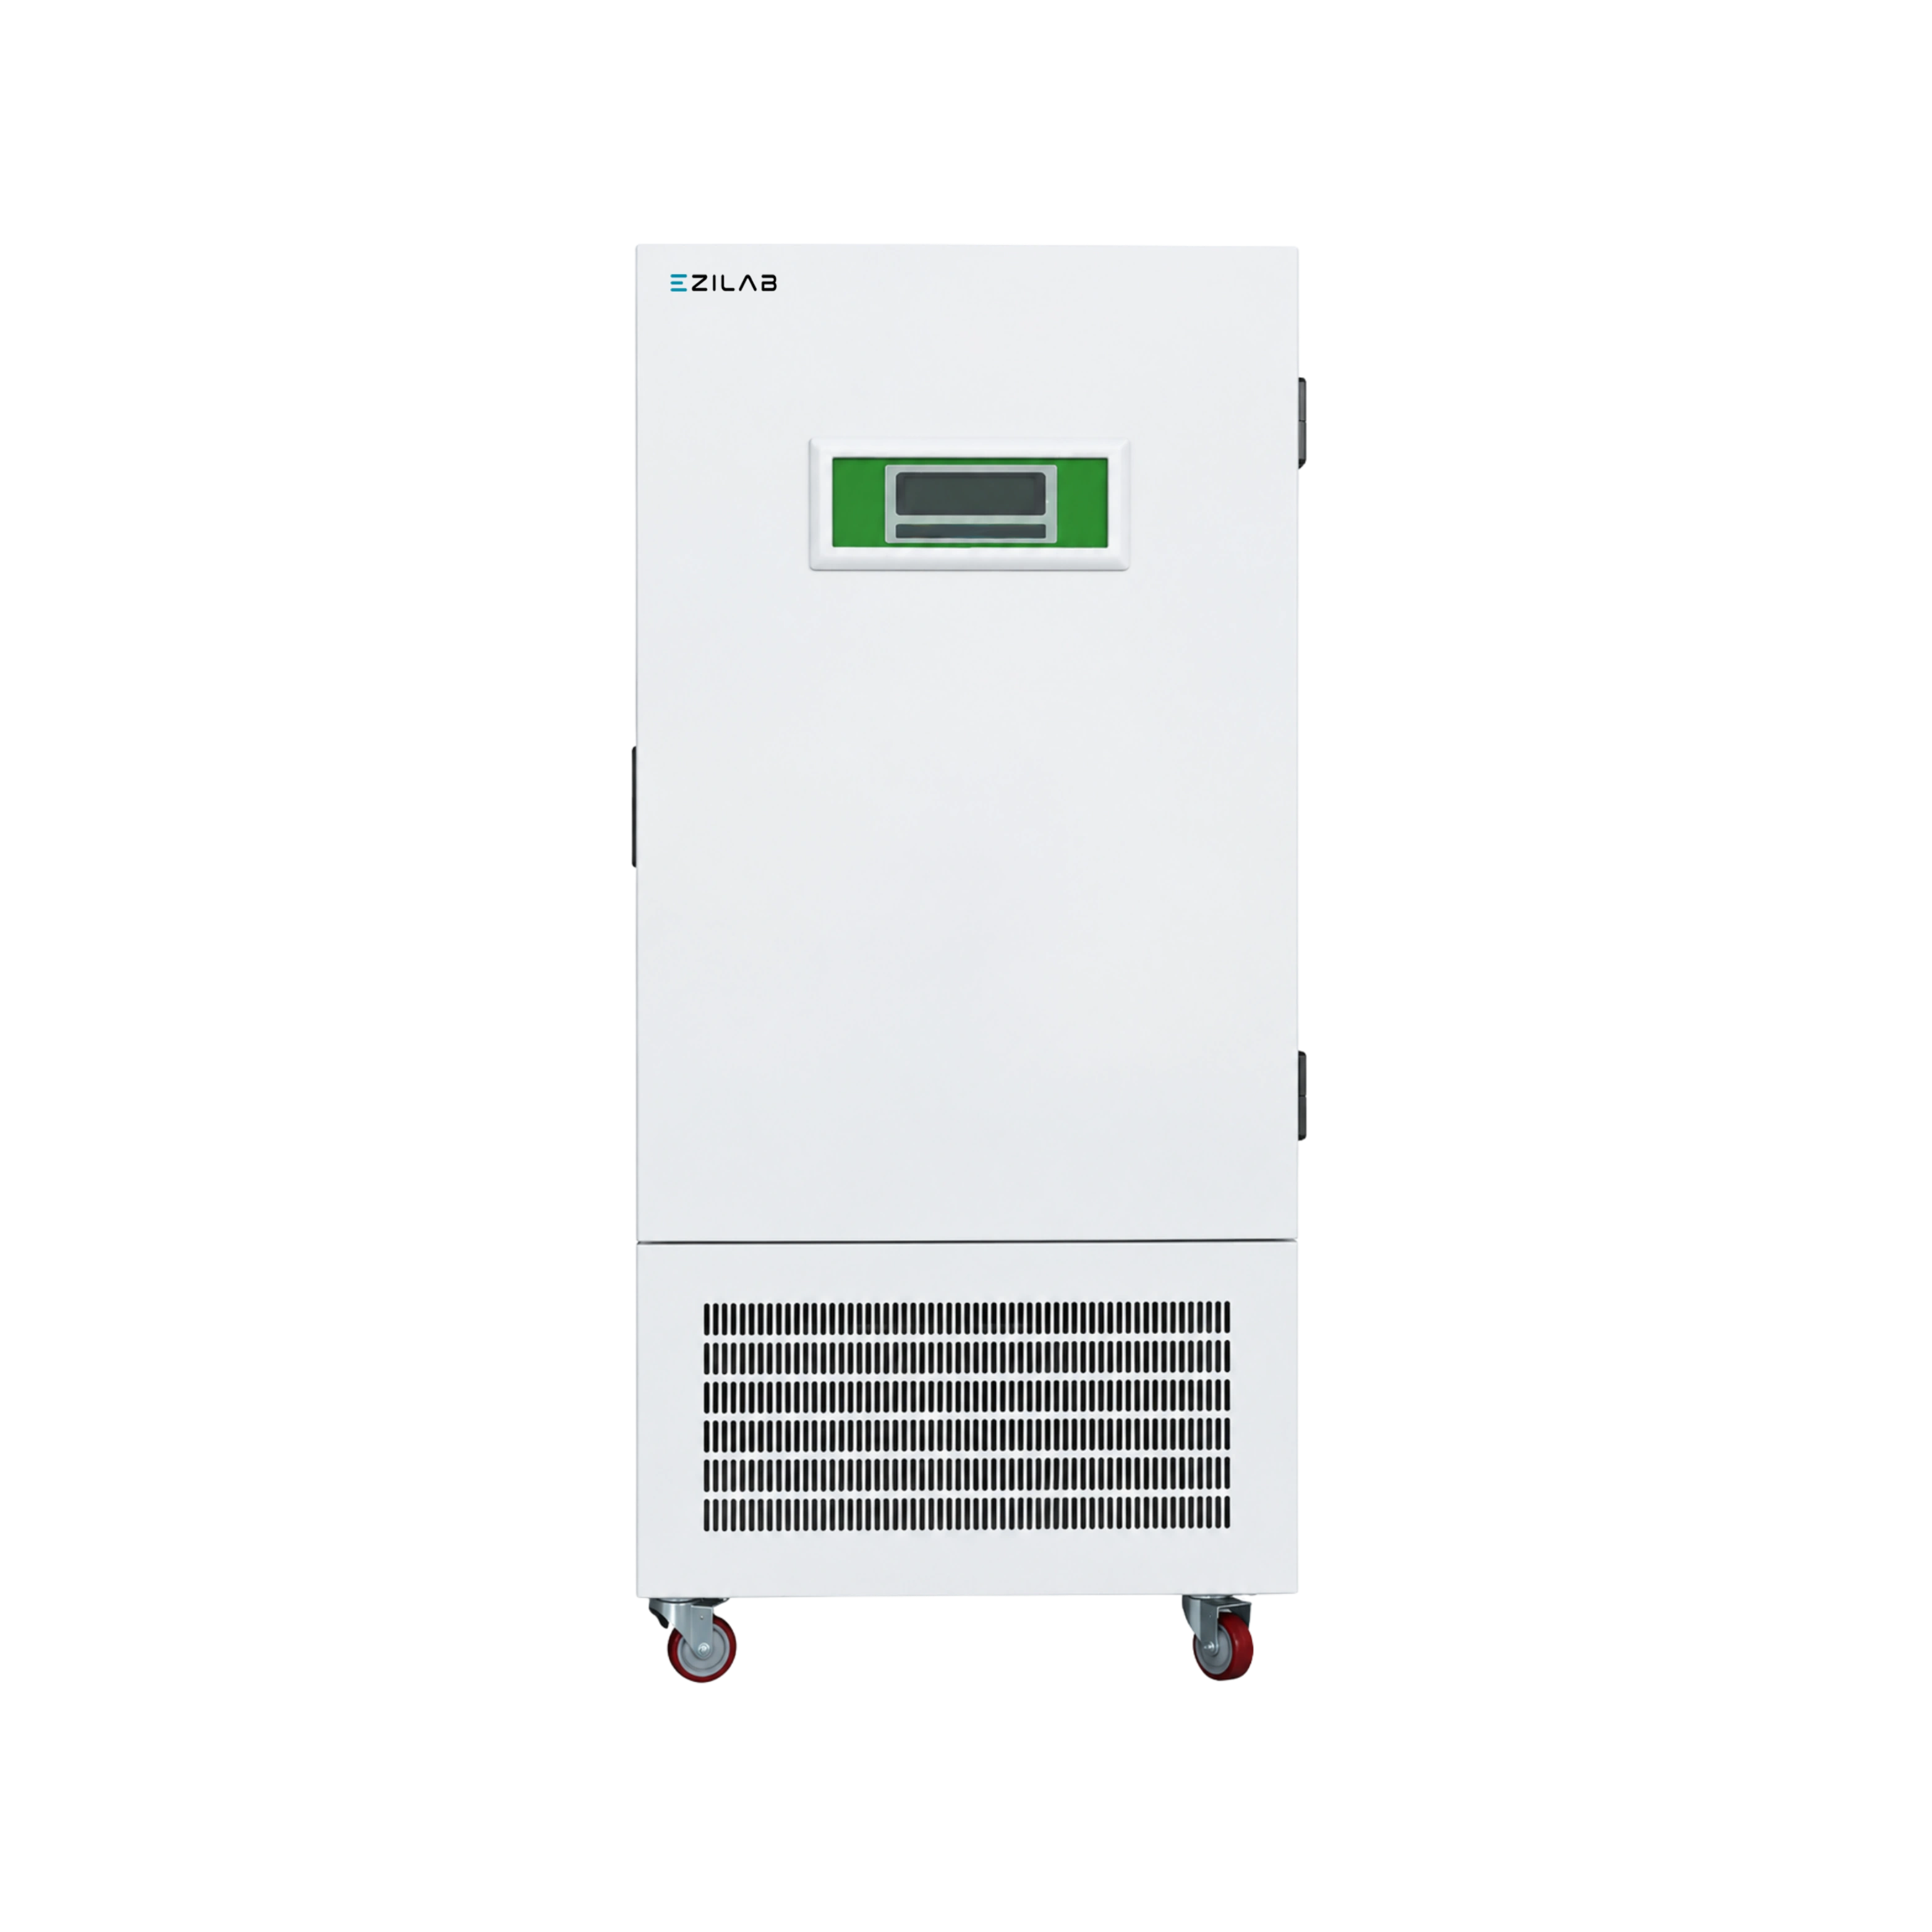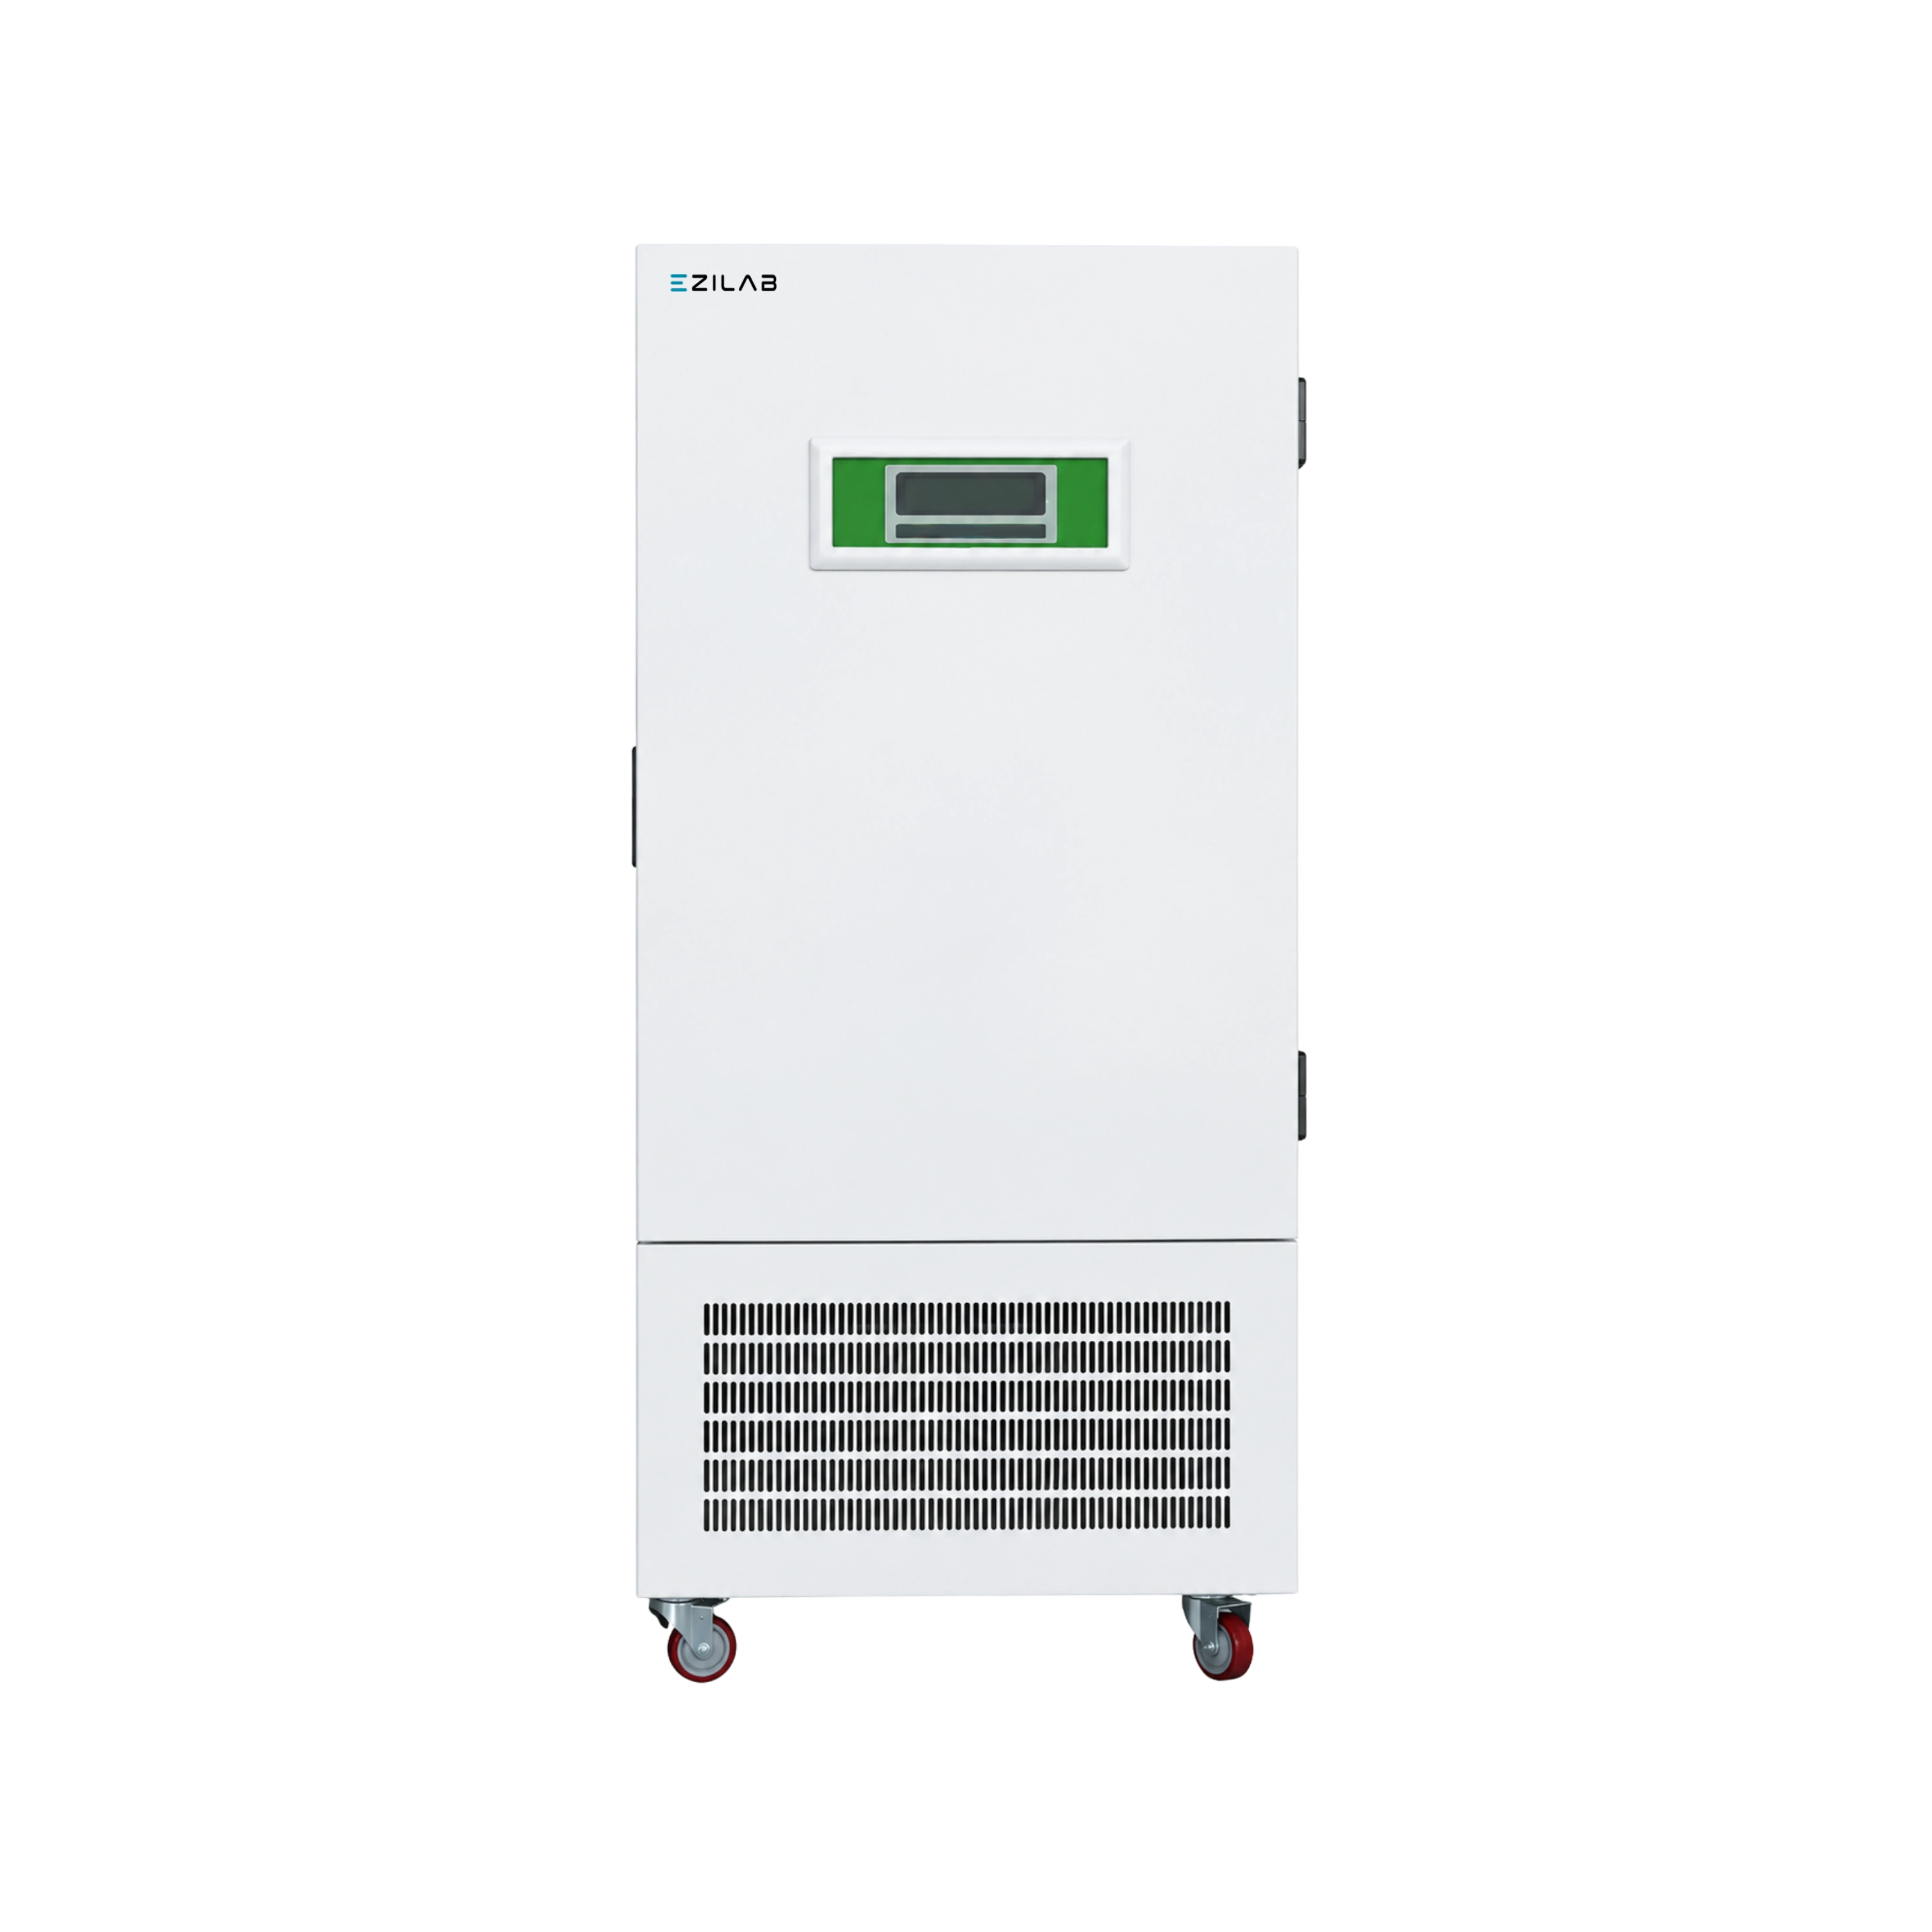
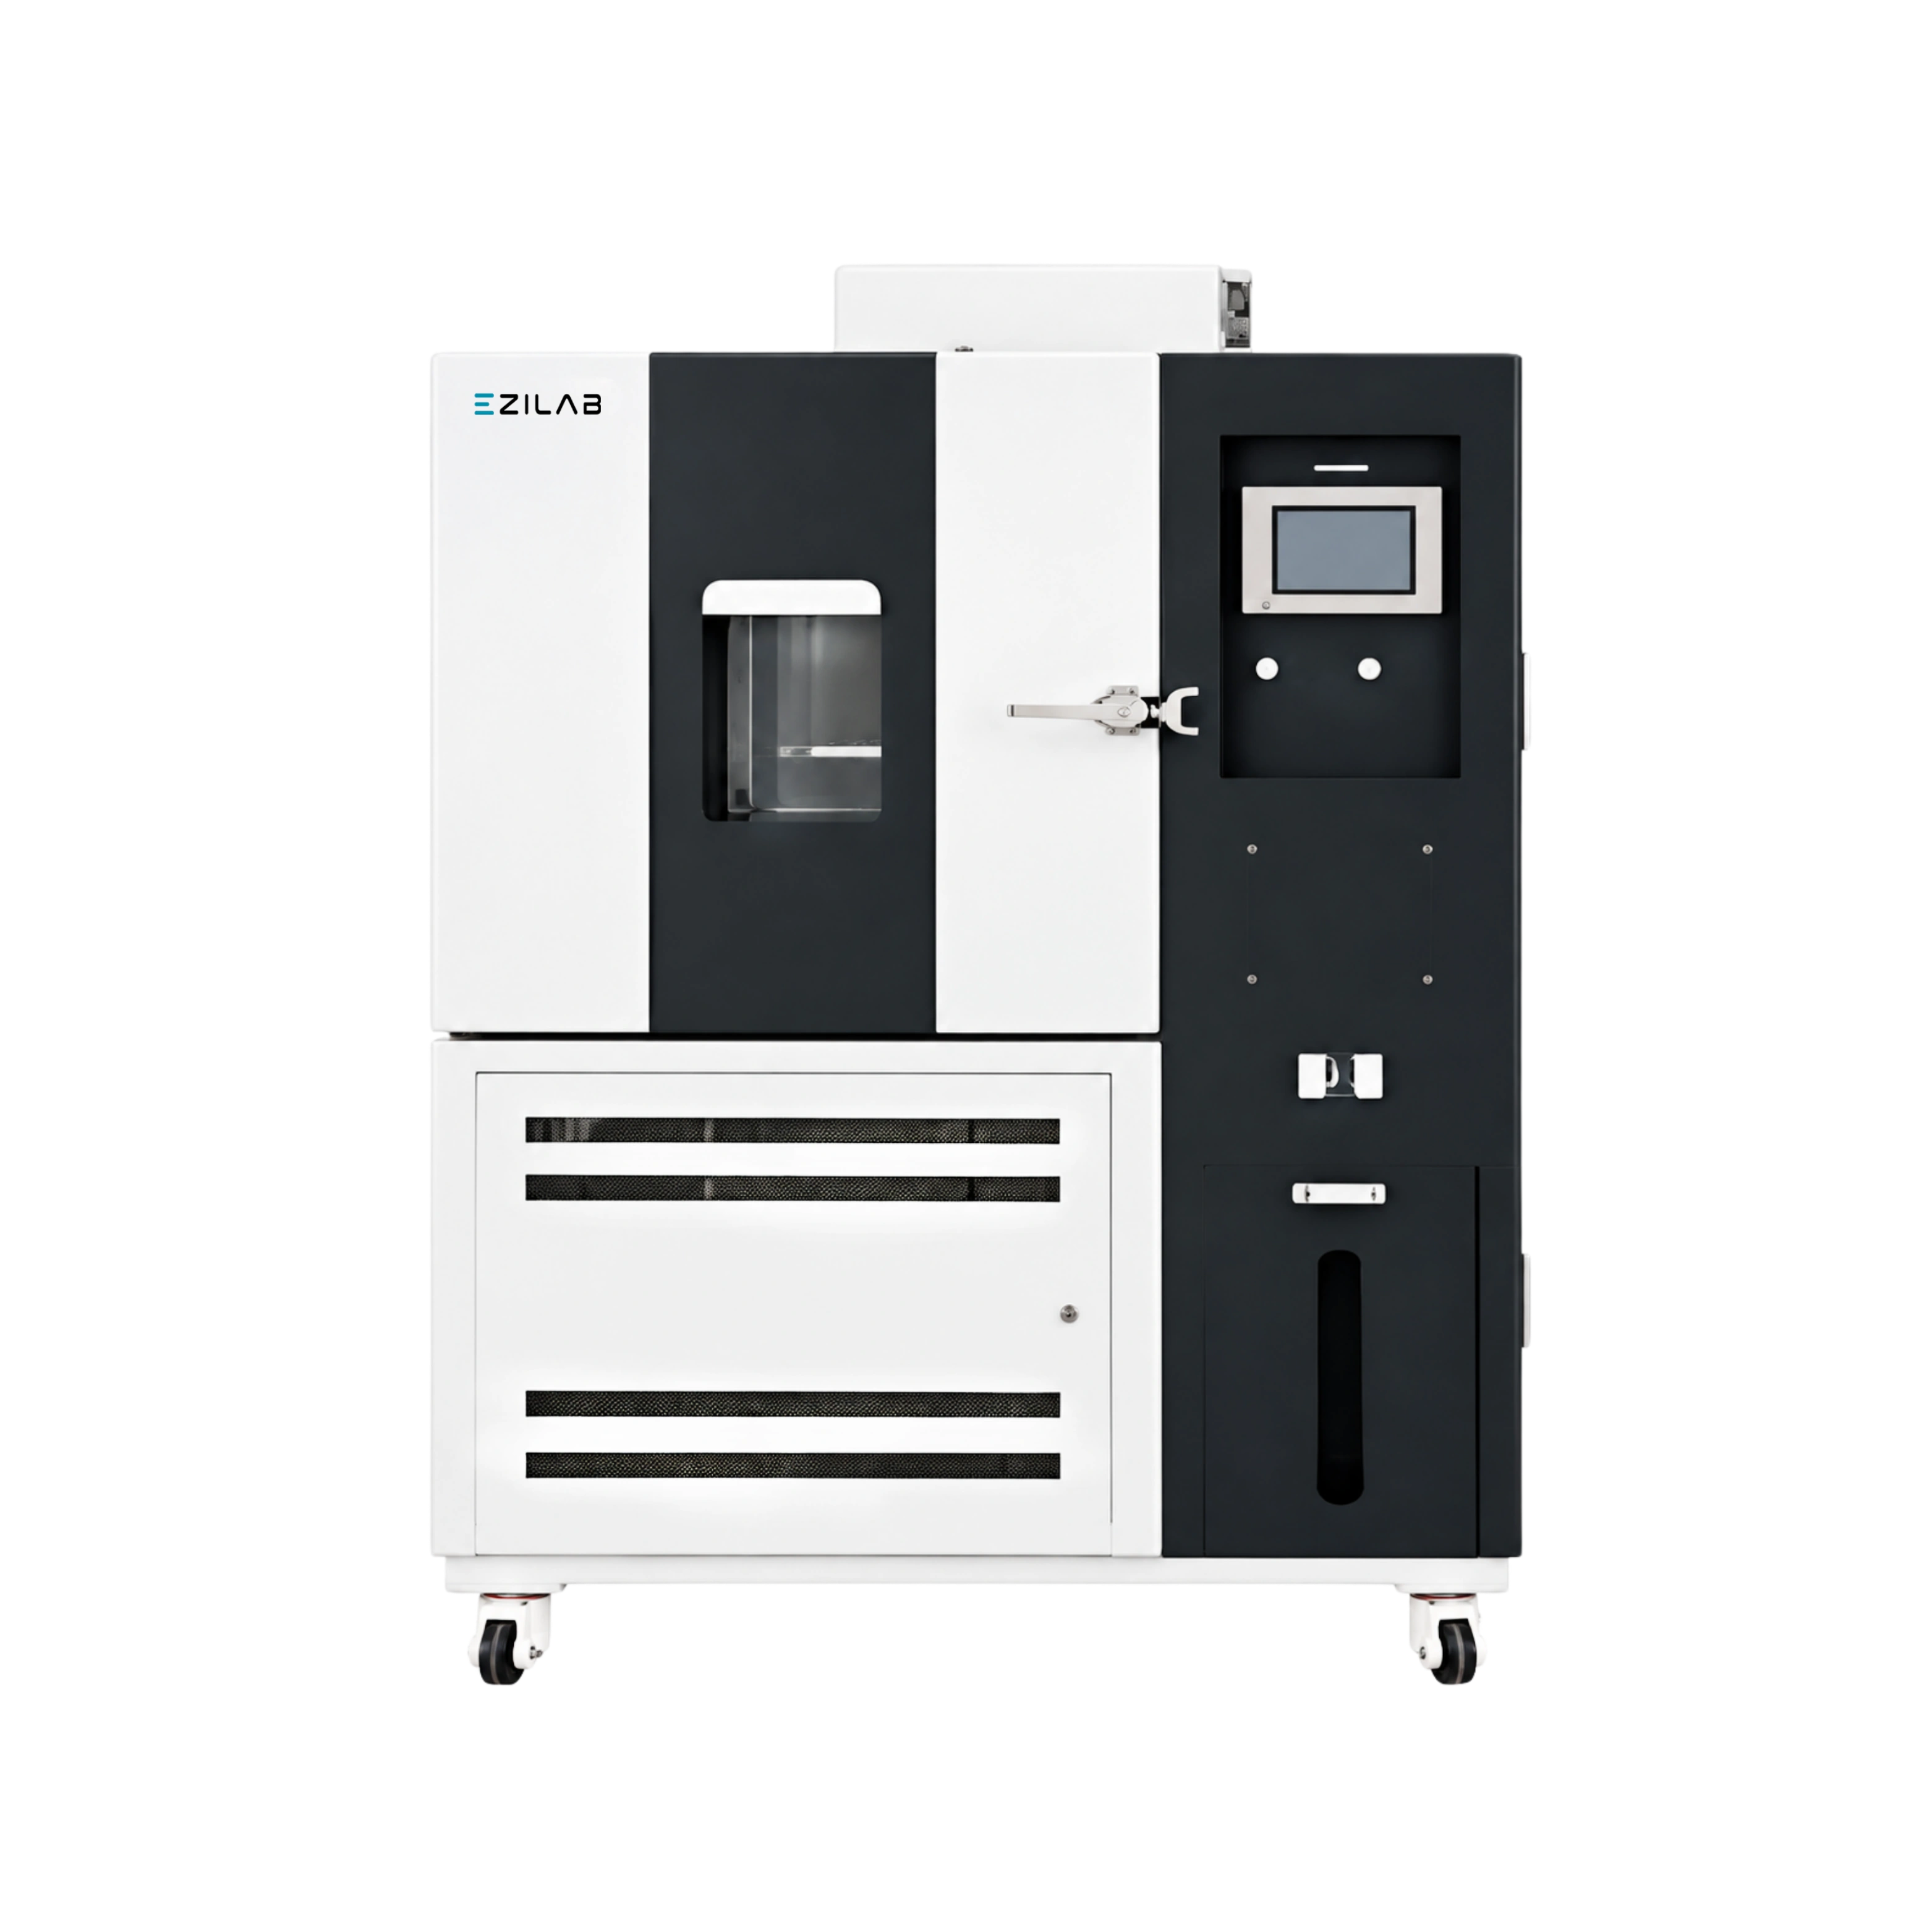
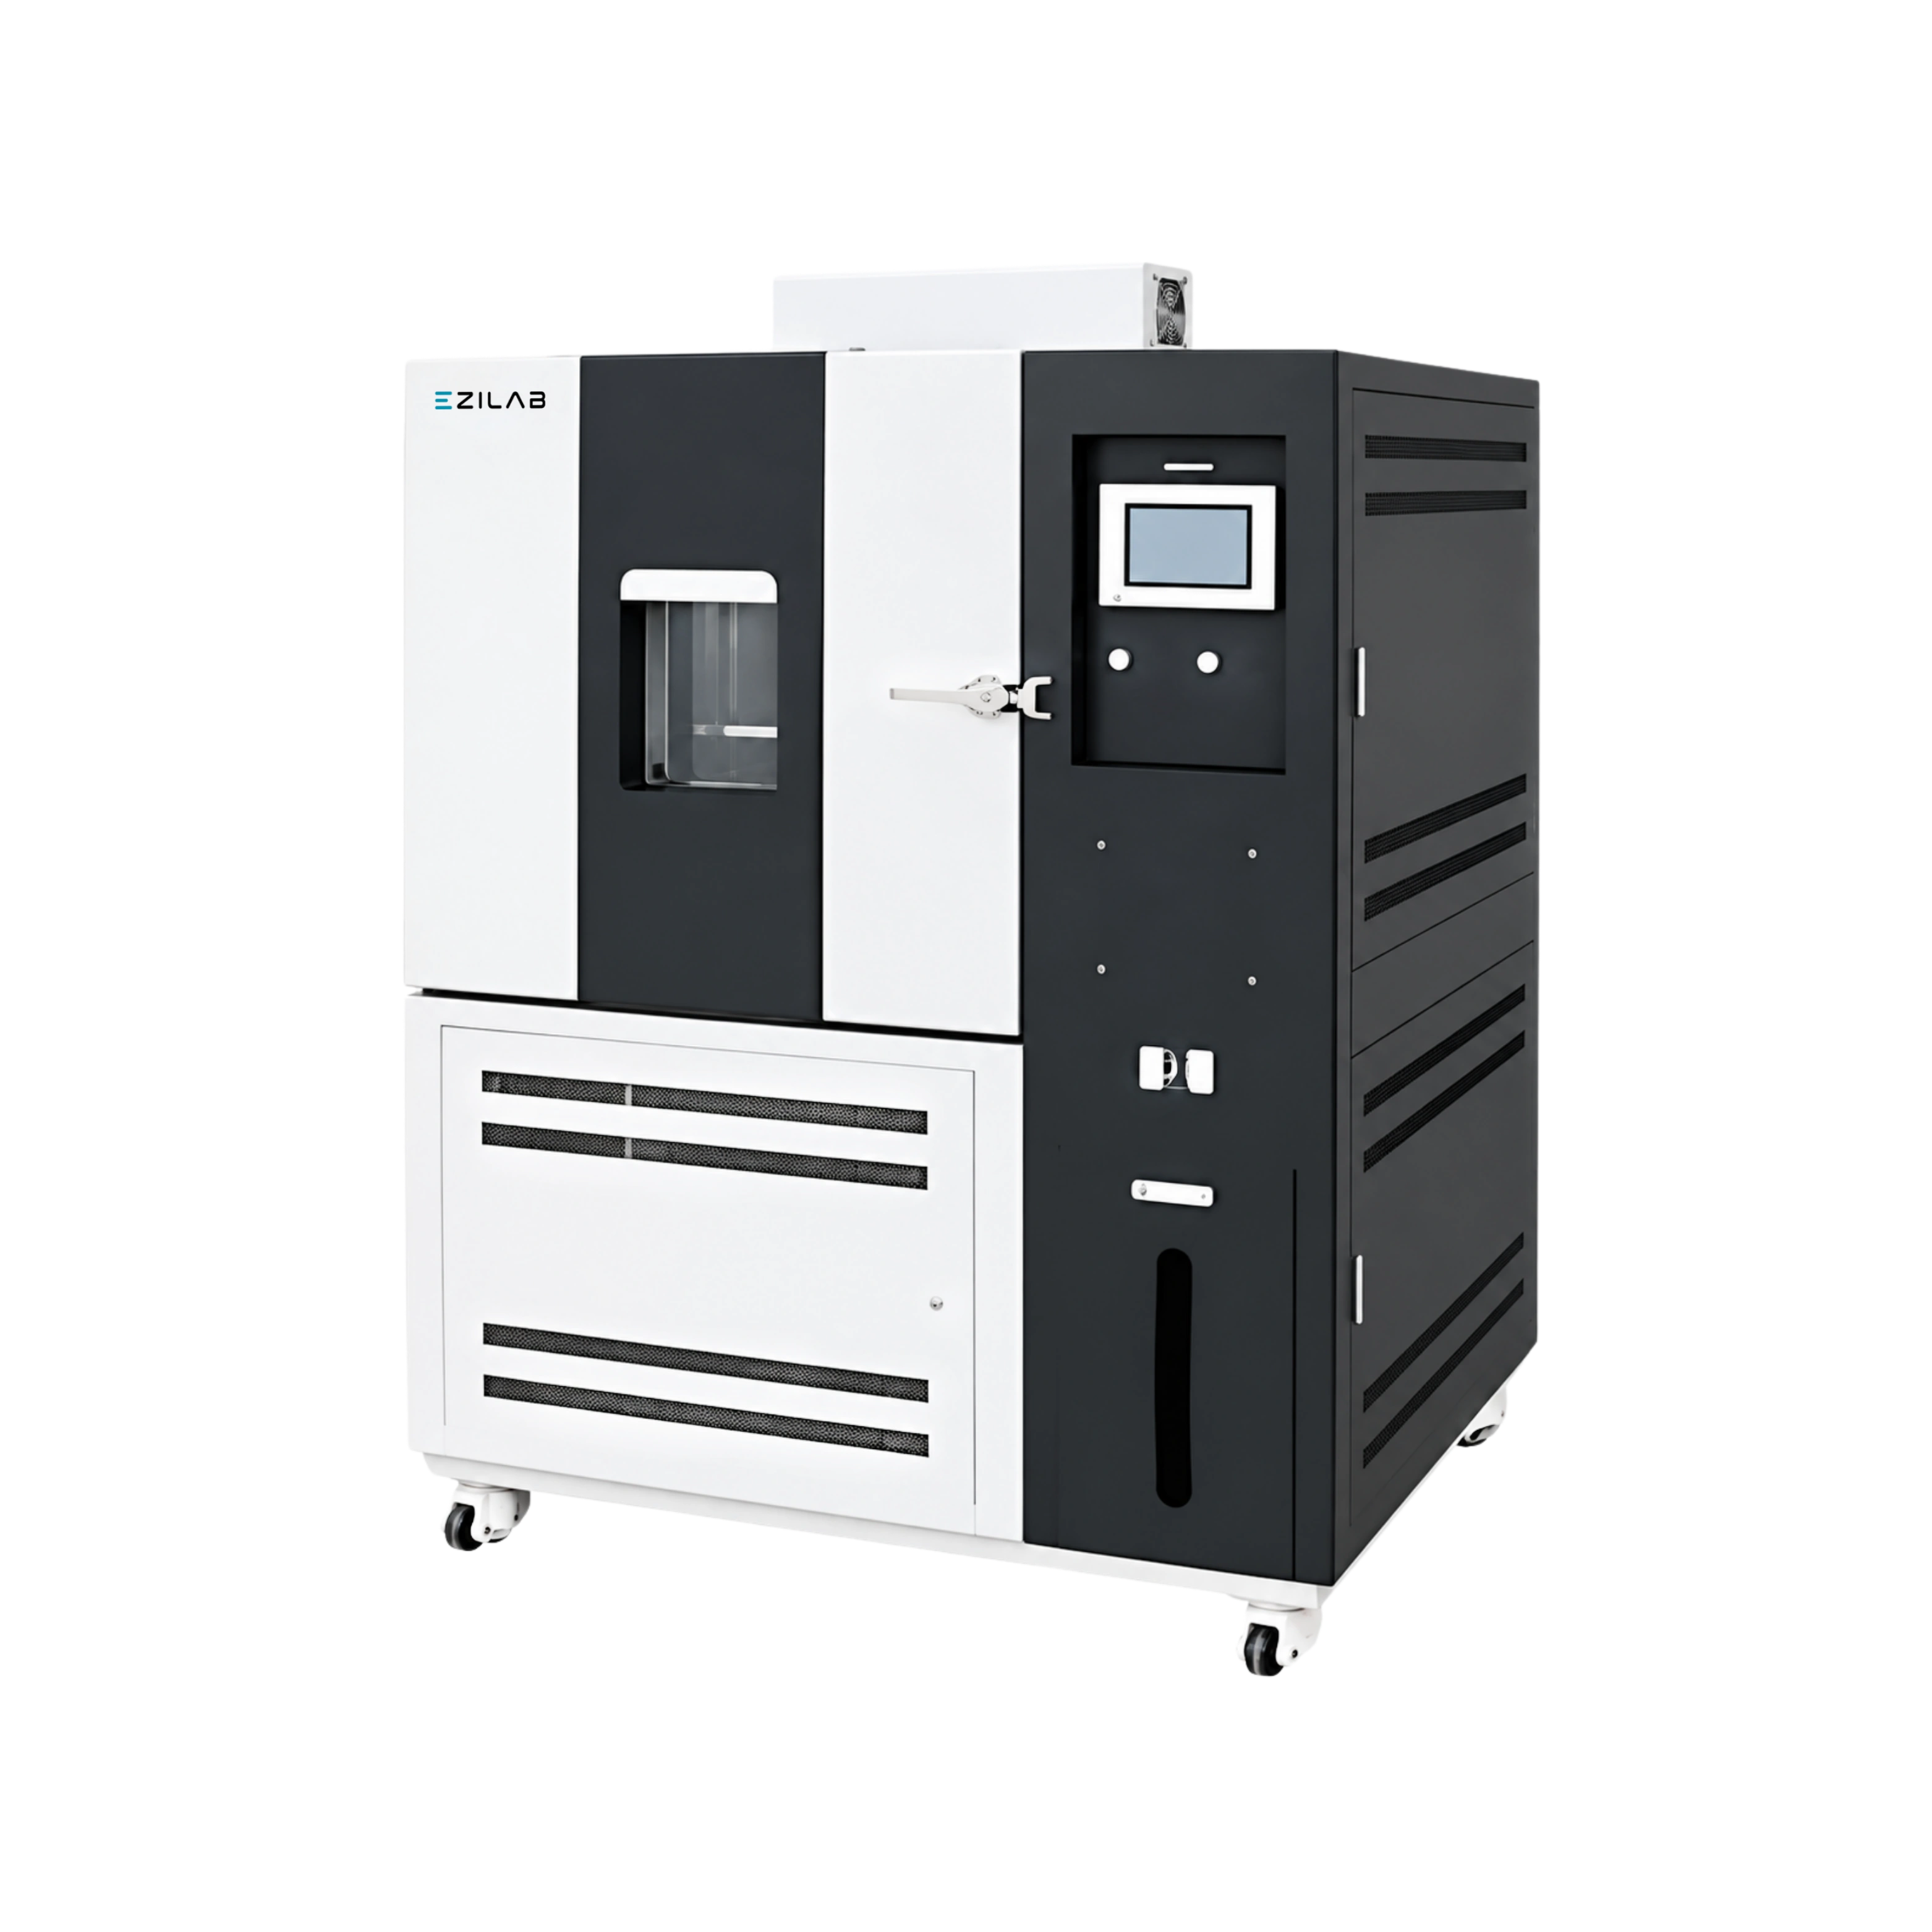
Ezilab's Stability Chamber EZL-SC513 serves pharmaceutical and research laboratories that need large-batch environmental stability testing with a wider humidity range than the standard 30-95% RH units in this line. At 392L capacity spanning 30-98% RH with programmable control, this stability test chamber covers pharmaceutical shelf-life studies and long-term product evaluation at a scale suited to full production batches rather than small sample runs. That 98% RH upper limit extends past the 90-95% ceiling on other chambers in this range, relevant for stability protocols testing product performance under near-saturation humidity conditions — packaging integrity, moisture-sensitive formulations, and products destined for genuinely humid climate zones where standard testing ranges don't fully represent real-world storage conditions. The 392L capacity sits close to the largest chamber in this line, giving pharmaceutical programs running multiple concurrent stability studies enough room to house several product batches simultaneously rather than scheduling studies sequentially through a smaller chamber. Programmable control lets labs set multi-step temperature and humidity profiles once and let extended studies run unattended across weeks or months, rather than manually adjusting conditions partway through a testing cycle. EziLab's Stability Test Chamber and Stability Chamber cover extended humidity-range stability testing needs across USA pharmaceutical laboratory settings.
| Chamber Capacity | 392 L |
|---|---|
| Temperature Range | -10°C to 120°C |
| Temperature Controller | Digital PID programmable controller |
| Humidity | 30% to 98%RH |
| Accuracy | ±3% |
| Shelves | 3 EA |
| Shelves Material | Adjustable stainless steel |
| Air-Convection | Tangent flow fan with AC motor |
| Inner Sight Lamp | Water proof AC30W lamp |
| Freezer | Air cooling unit system |
| Door | Silicone door |
| Internal Material | Stainless steel |
| External Material | Steel plate with powder coating |
| Power | AC 220V, 50/60Hz, 1-phase |
| Internal Dimension (W×D×H) | 700×700×800 mm |
| External Dimension (W×D×H) | 1200×1100×1900 mm |
Optimum performance with advanced features
Tangent air flow design provides precise uniformity
Energy efficient, lower power draw
Quiet operation
Adjustable steel shelves
Castors for easy mobility
Lockable doors
5.7” LCD touch screen for easy operation
Visual and audible alarm functions
High-efficiency equipment for electronic industry
These are developed to meet the requirements of test laboratories in pharmaceutical industries, electronic industries, quality assurance and chemical industries etc.