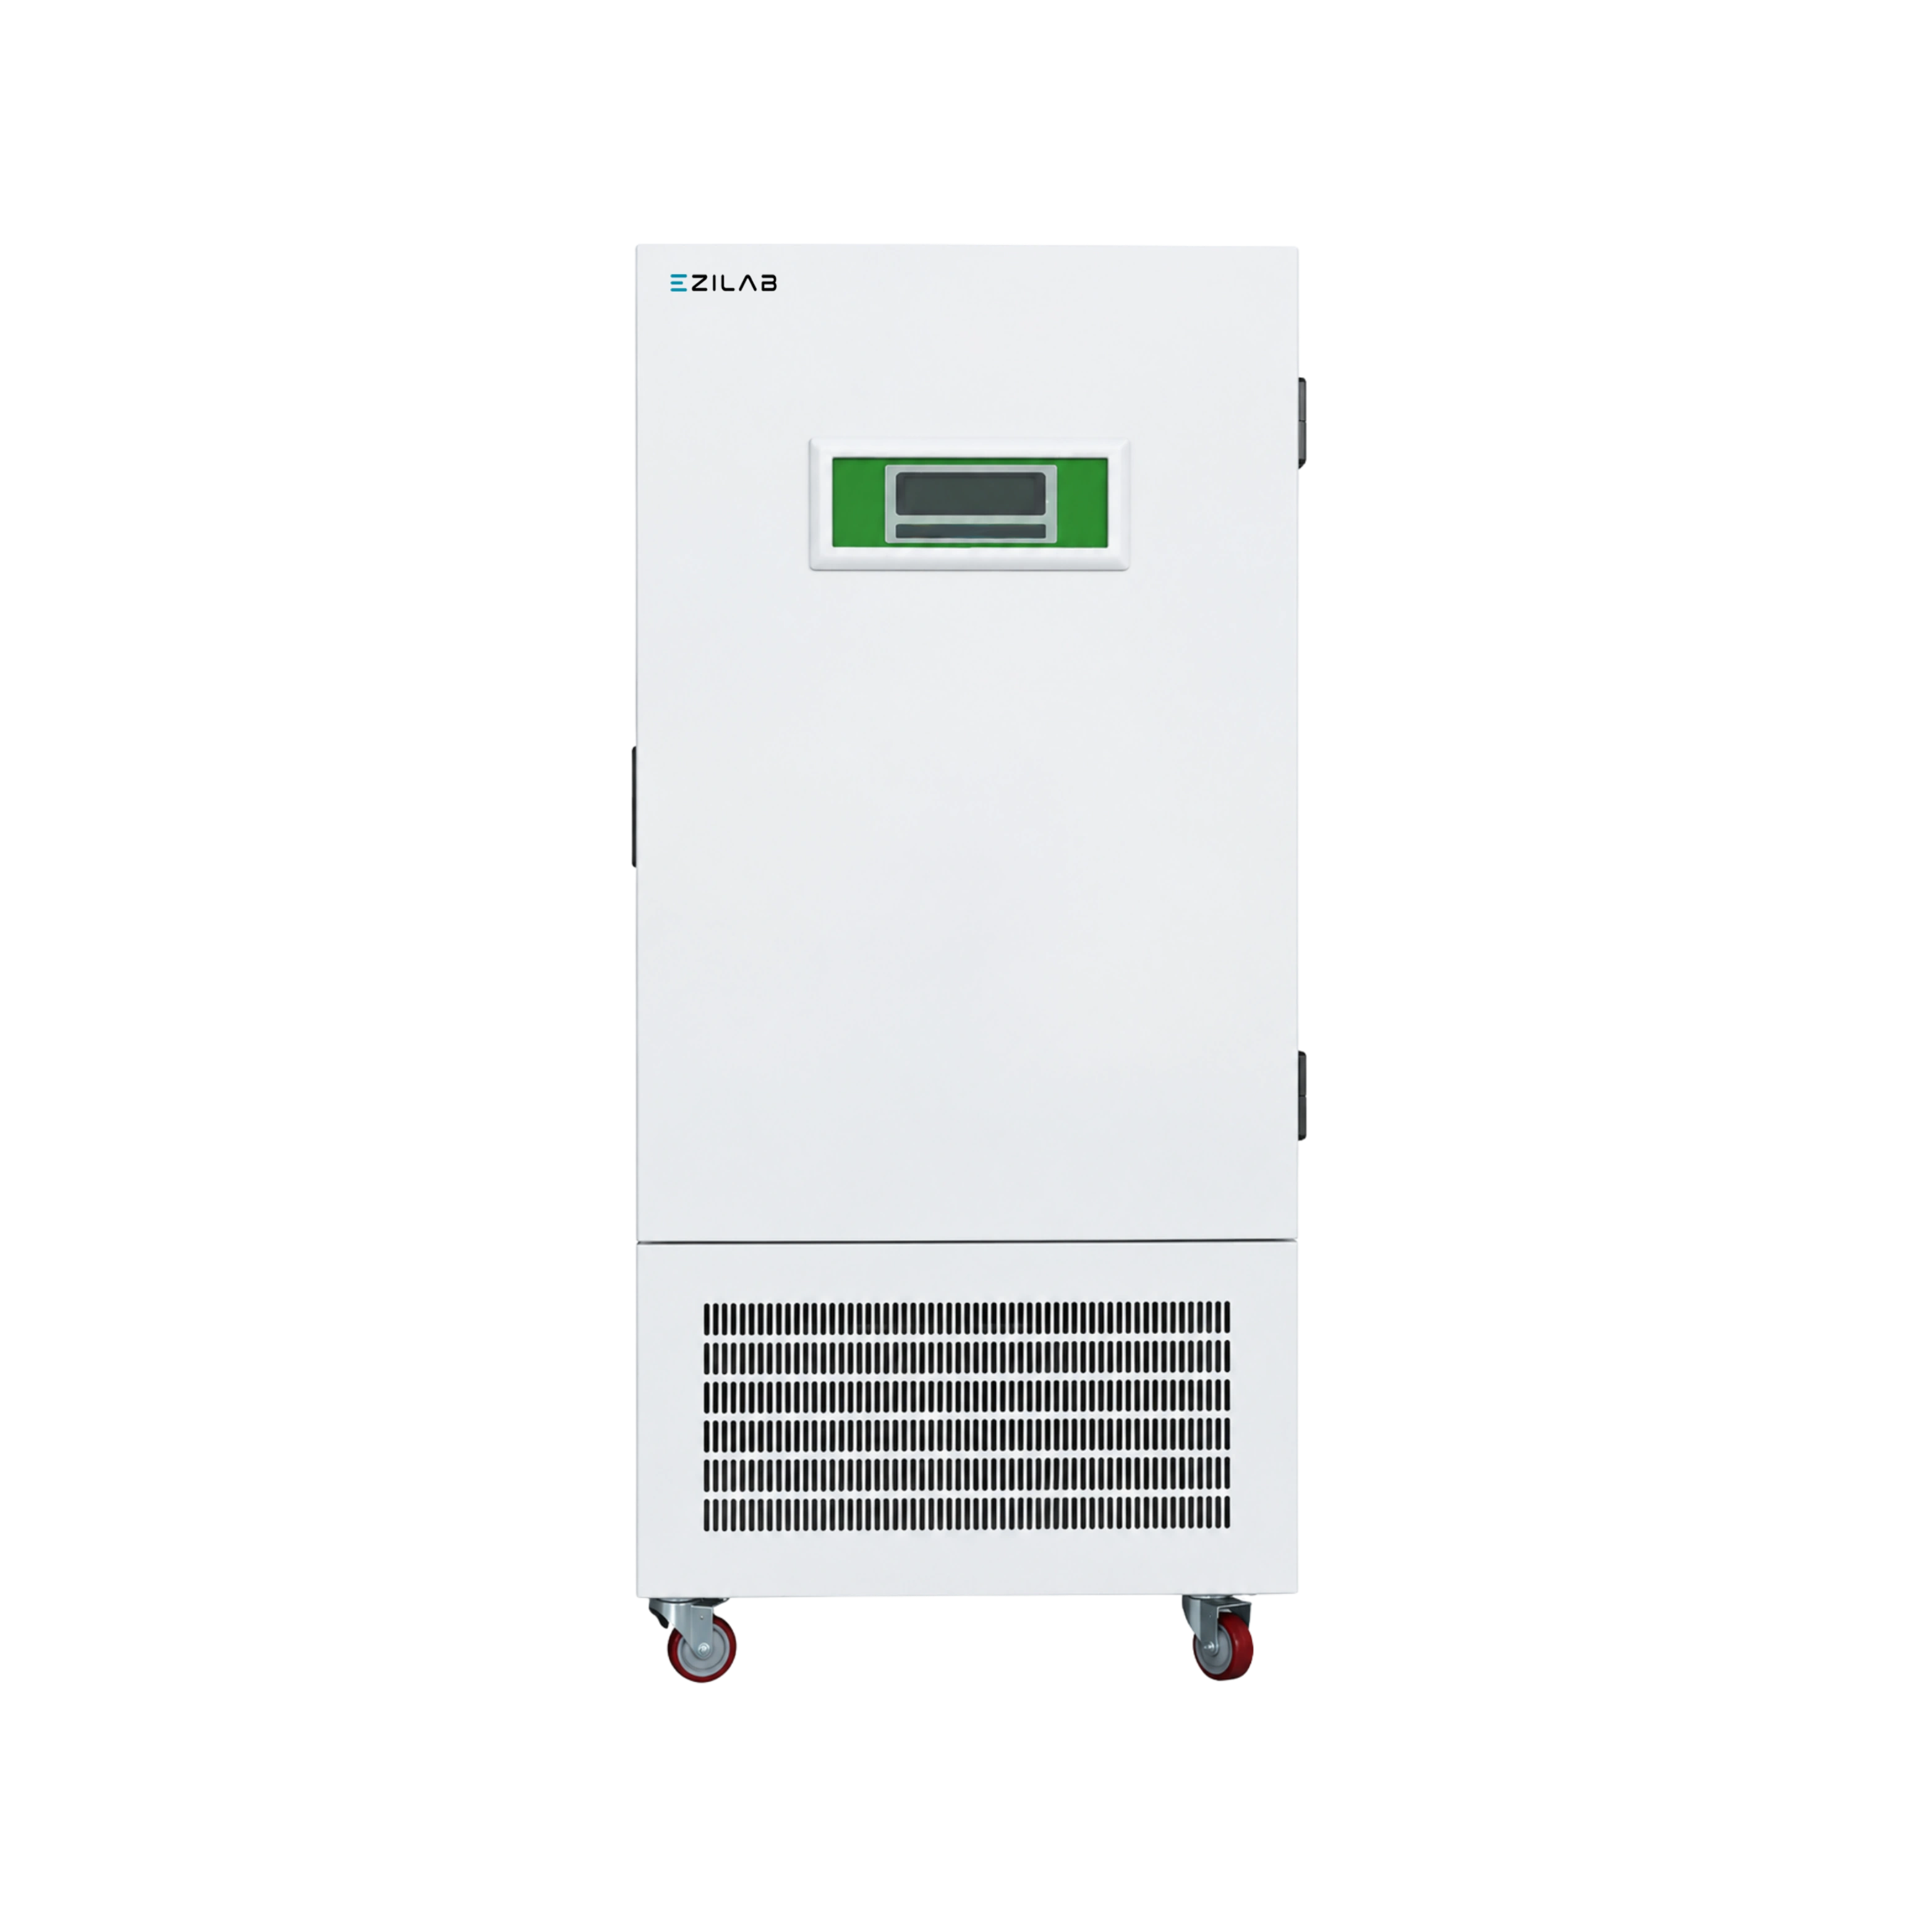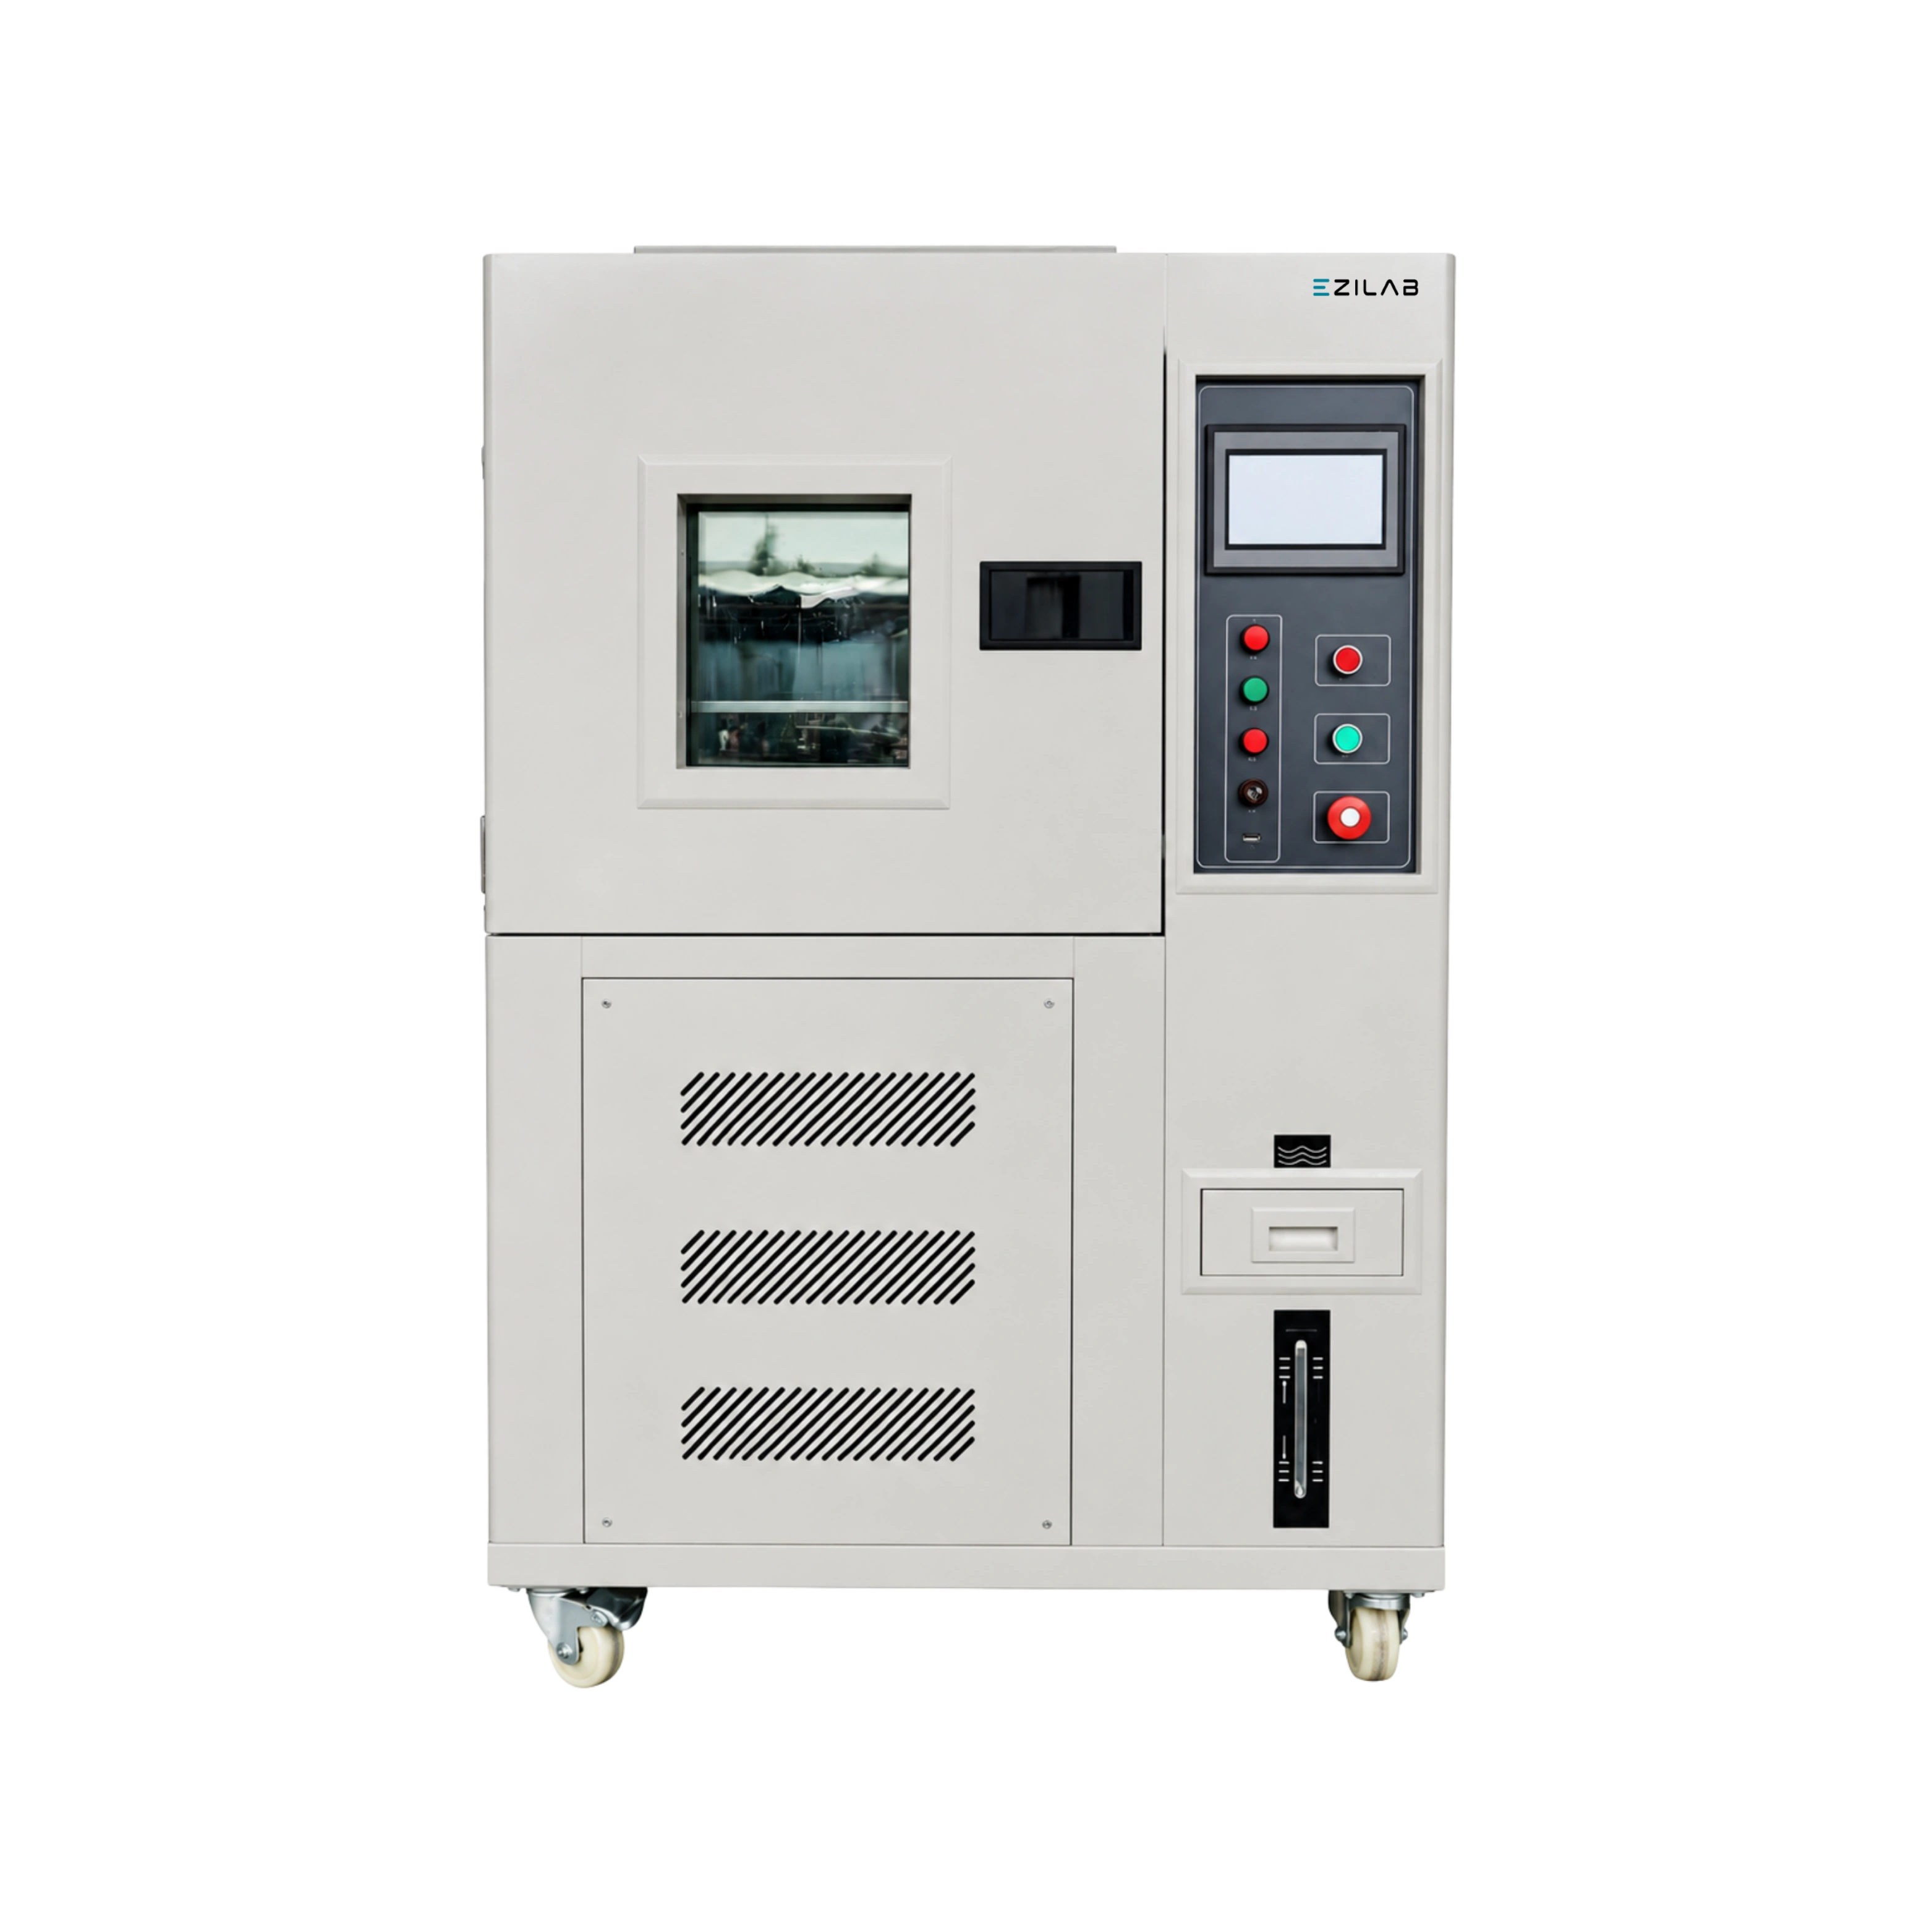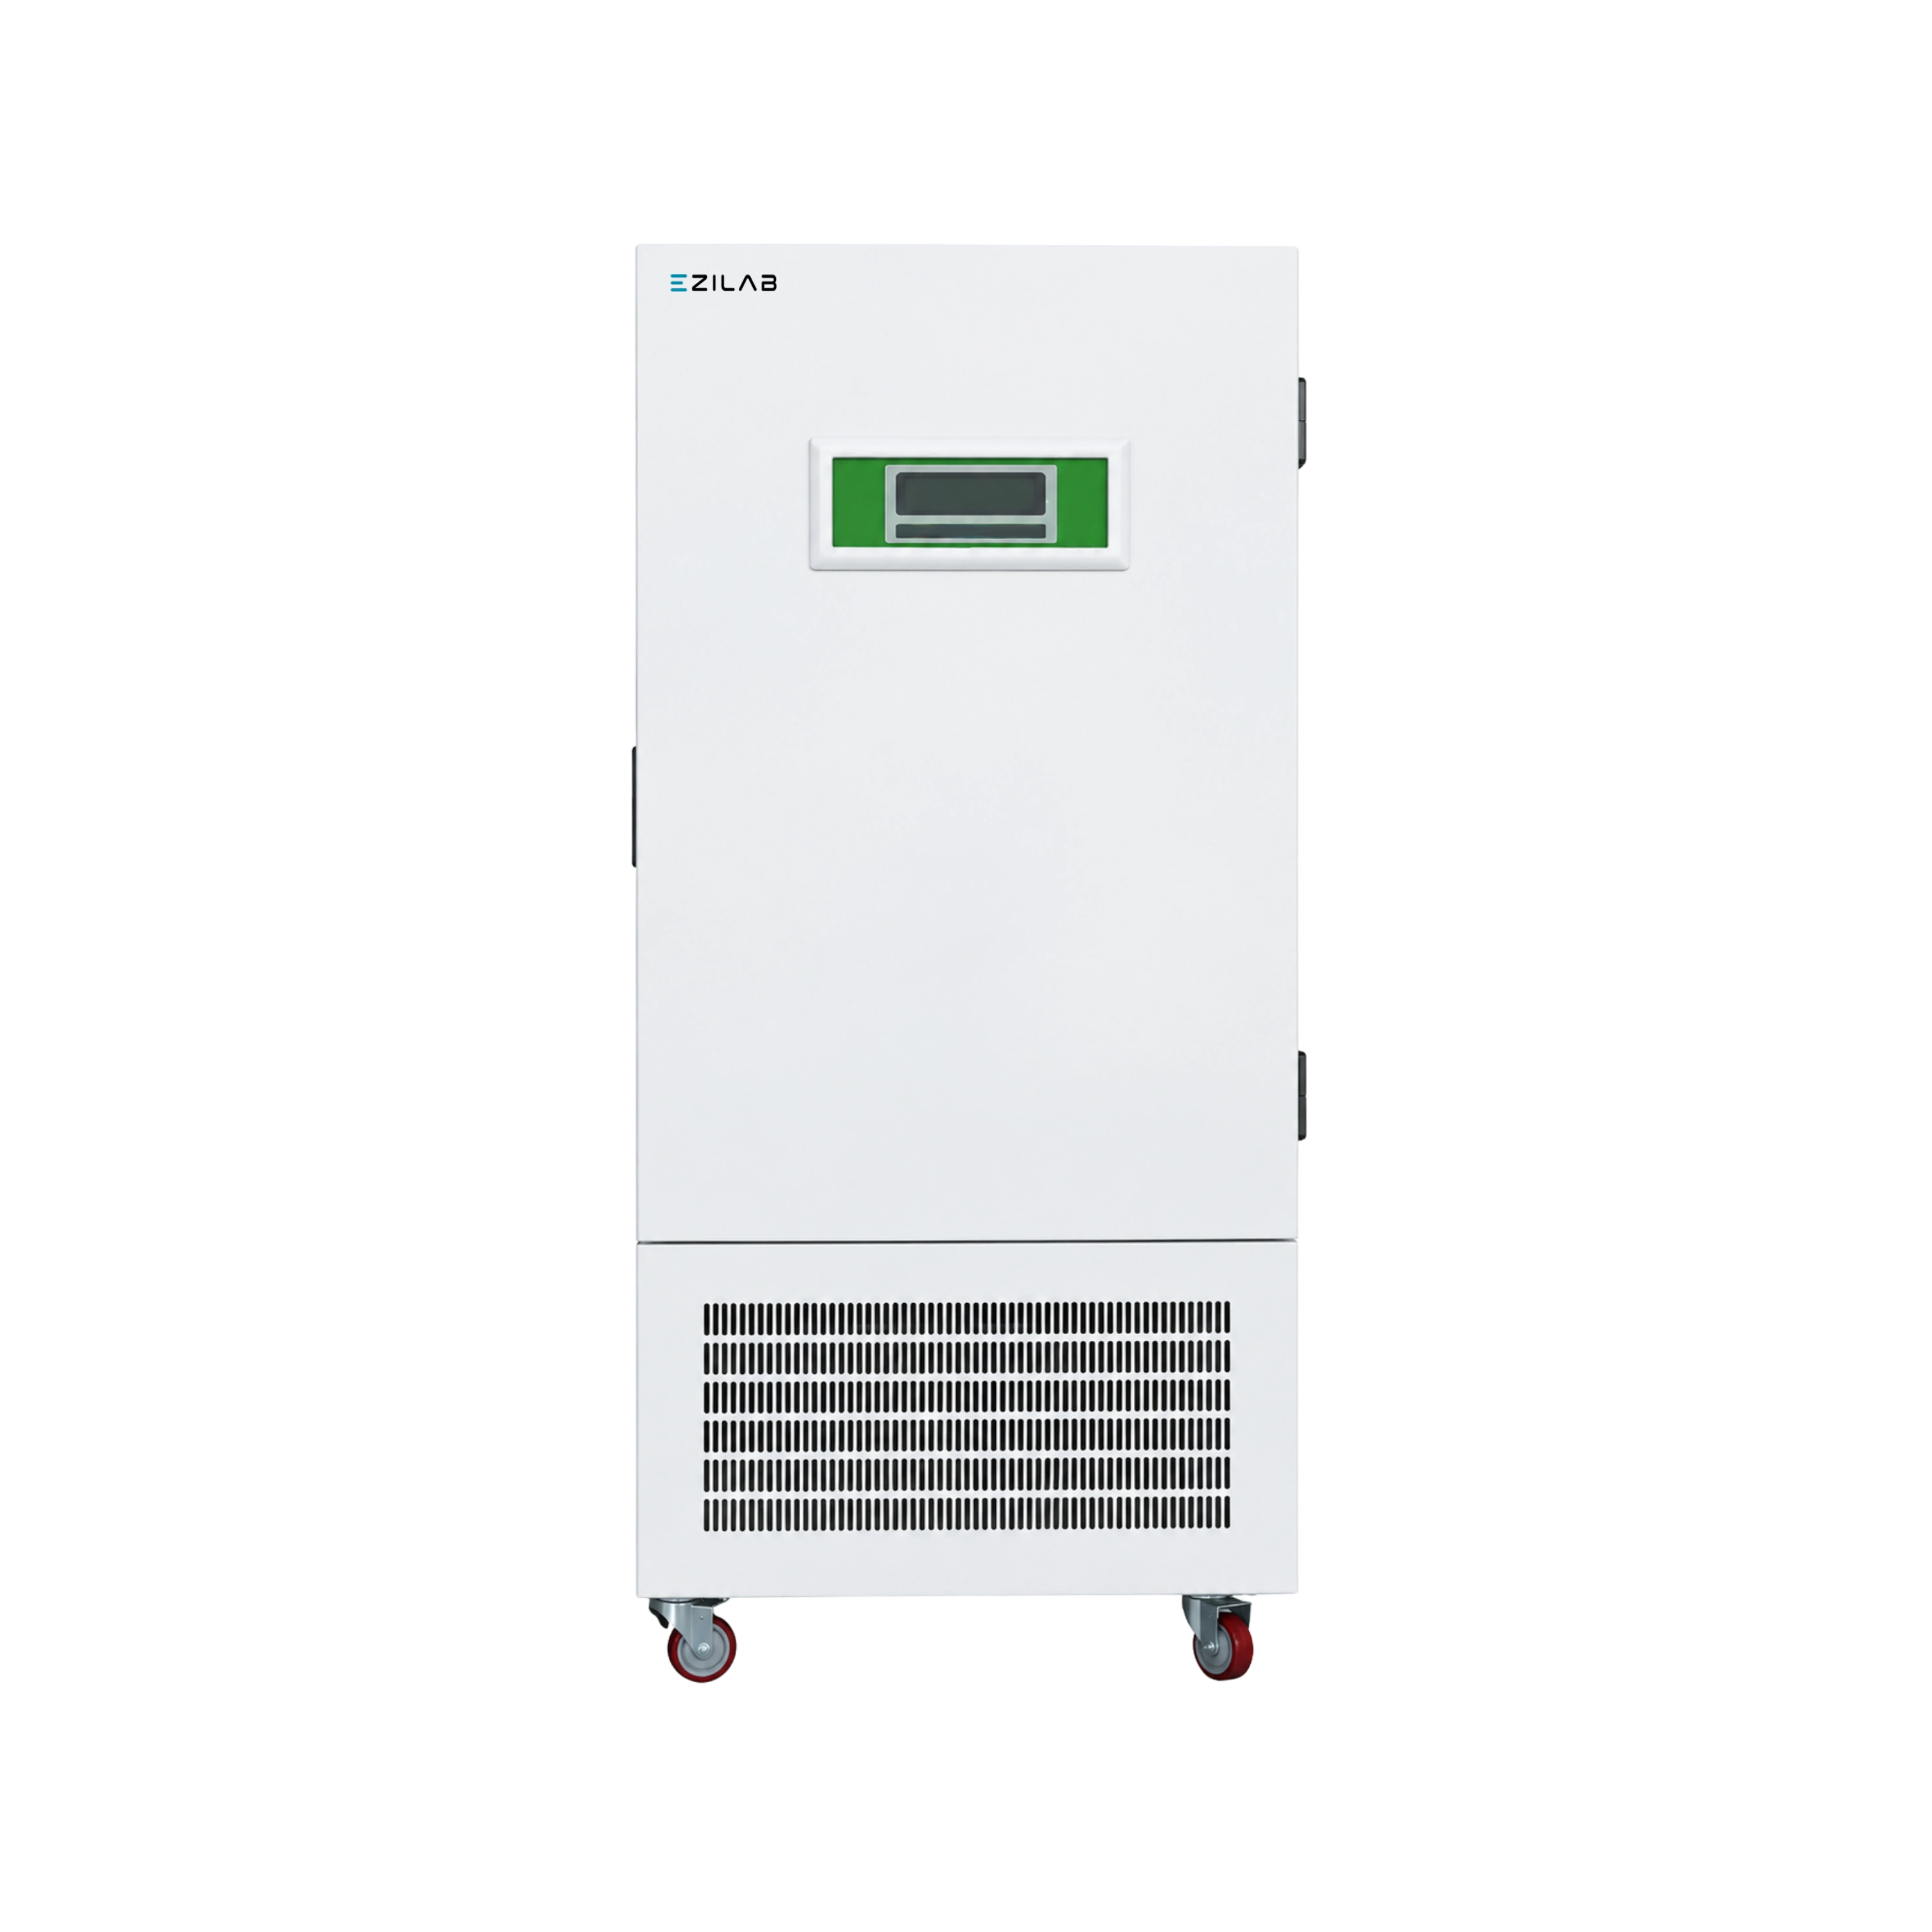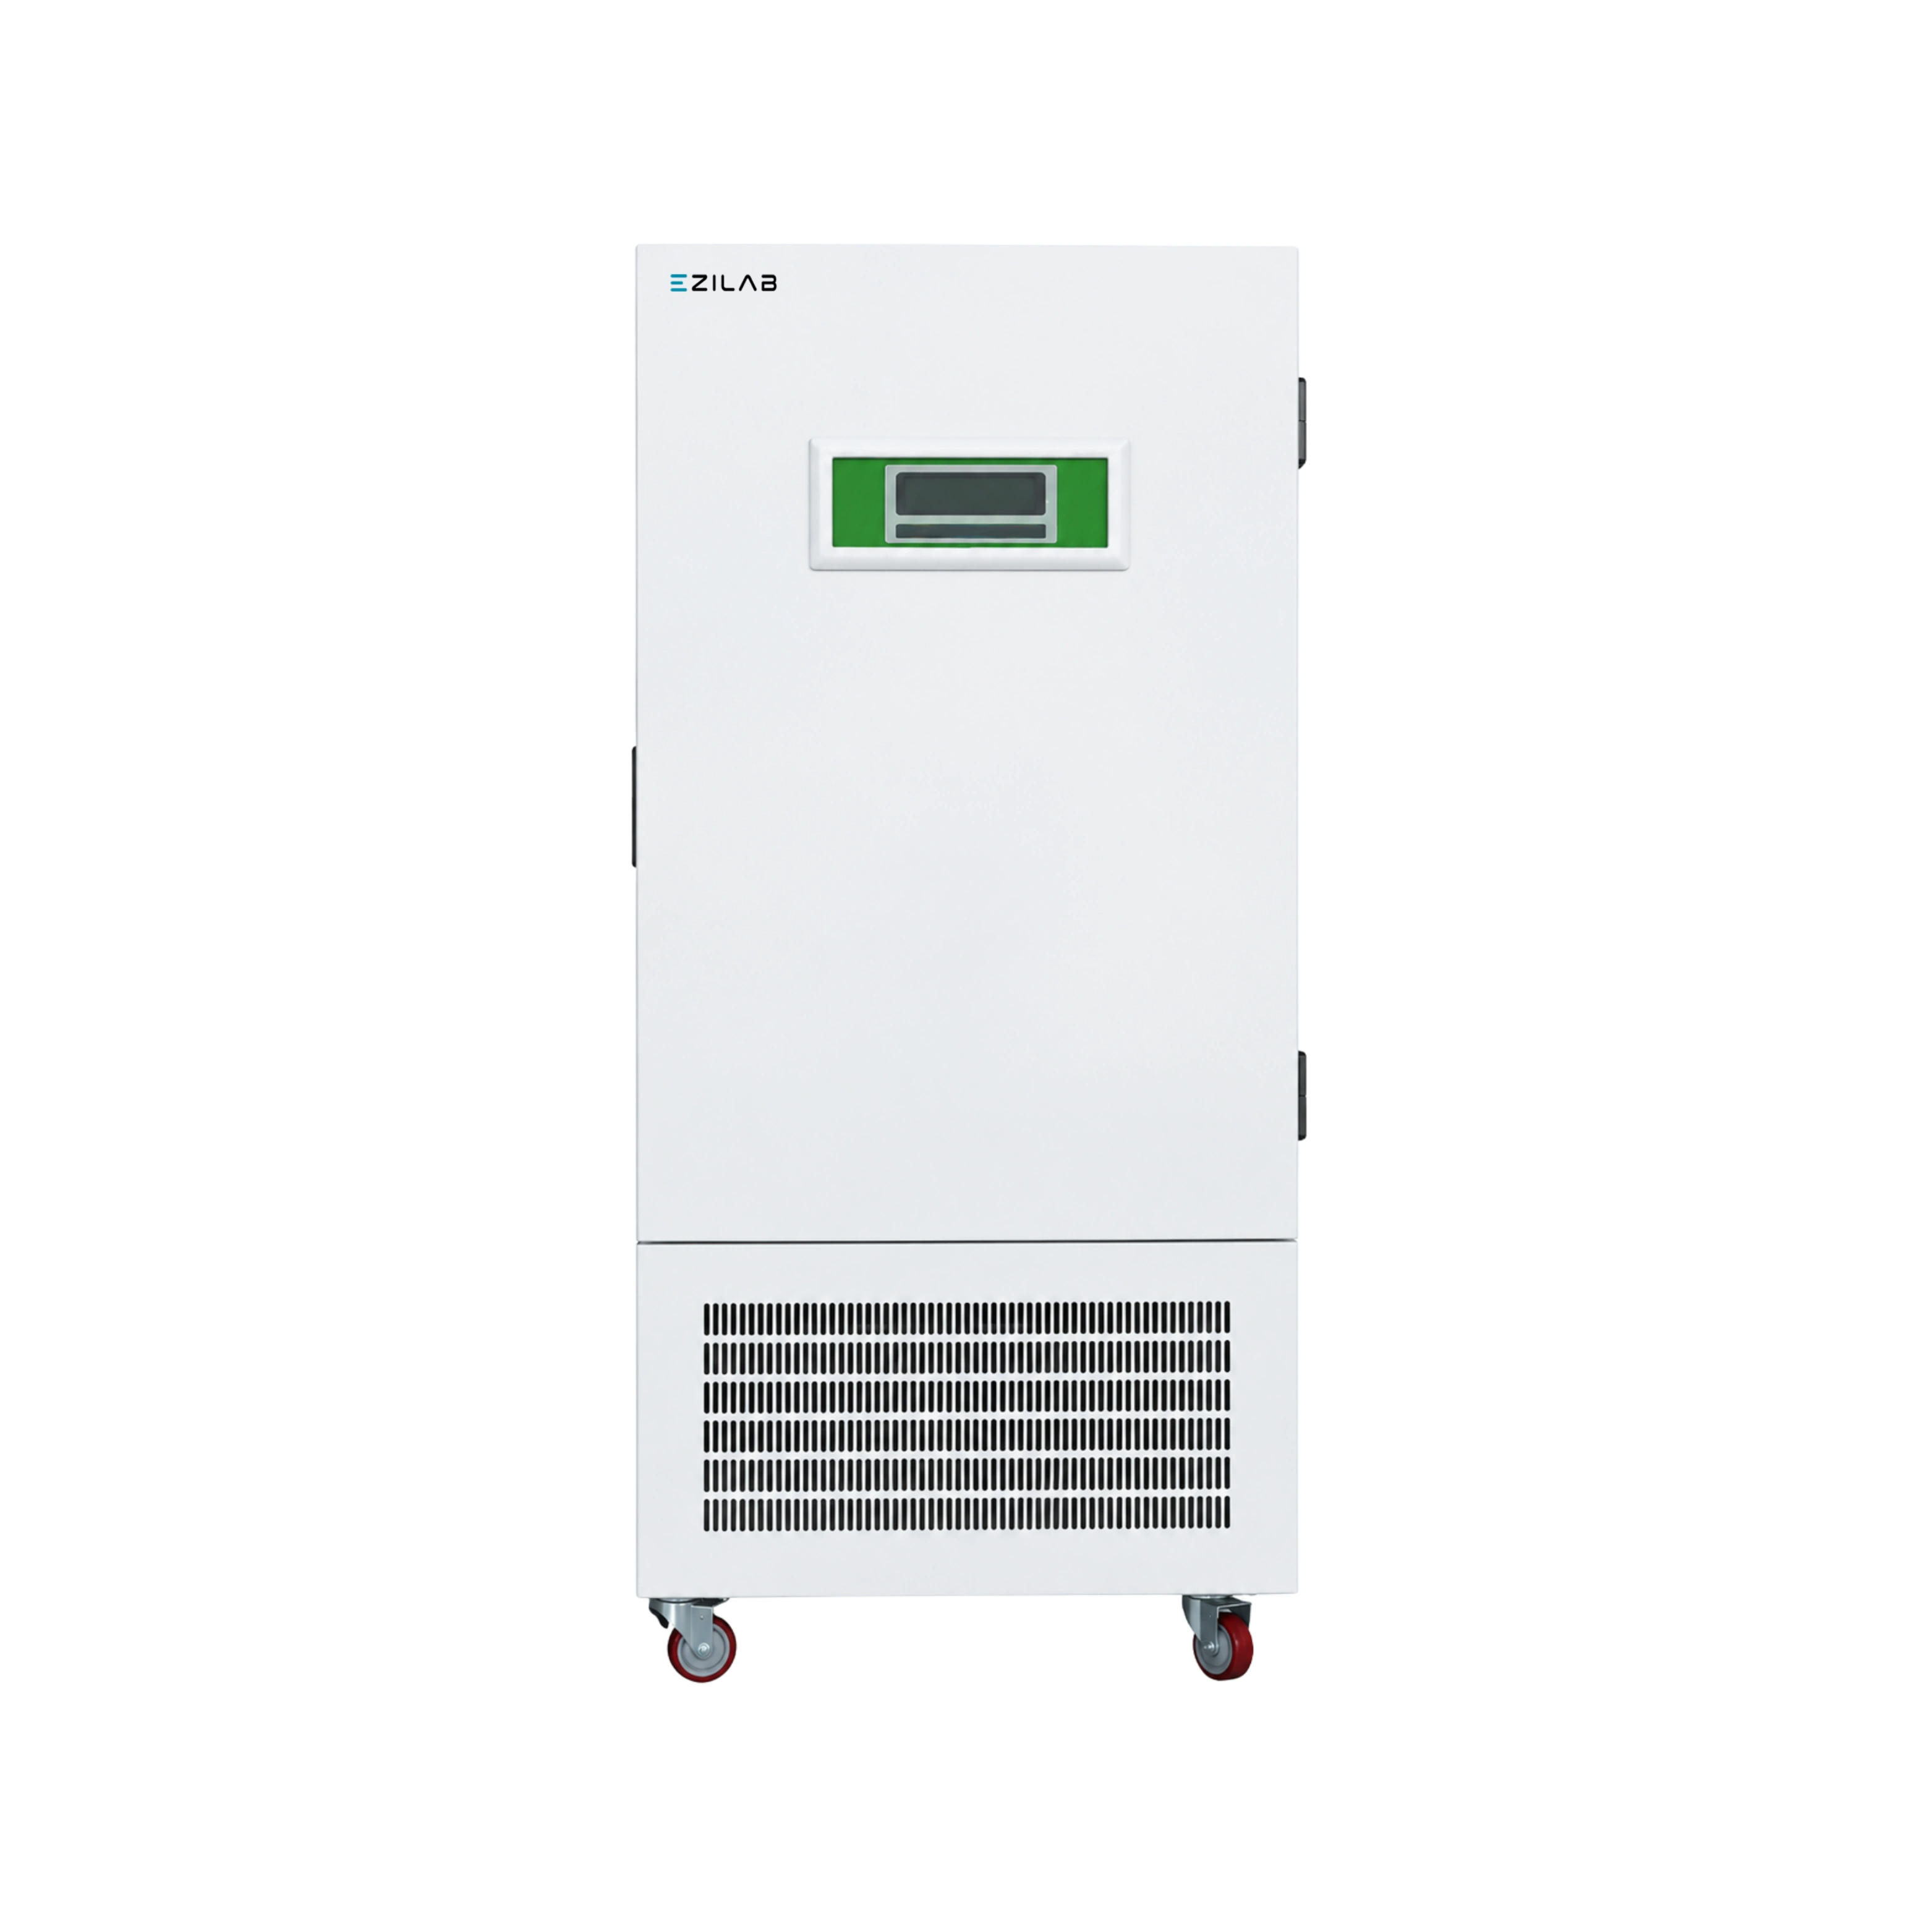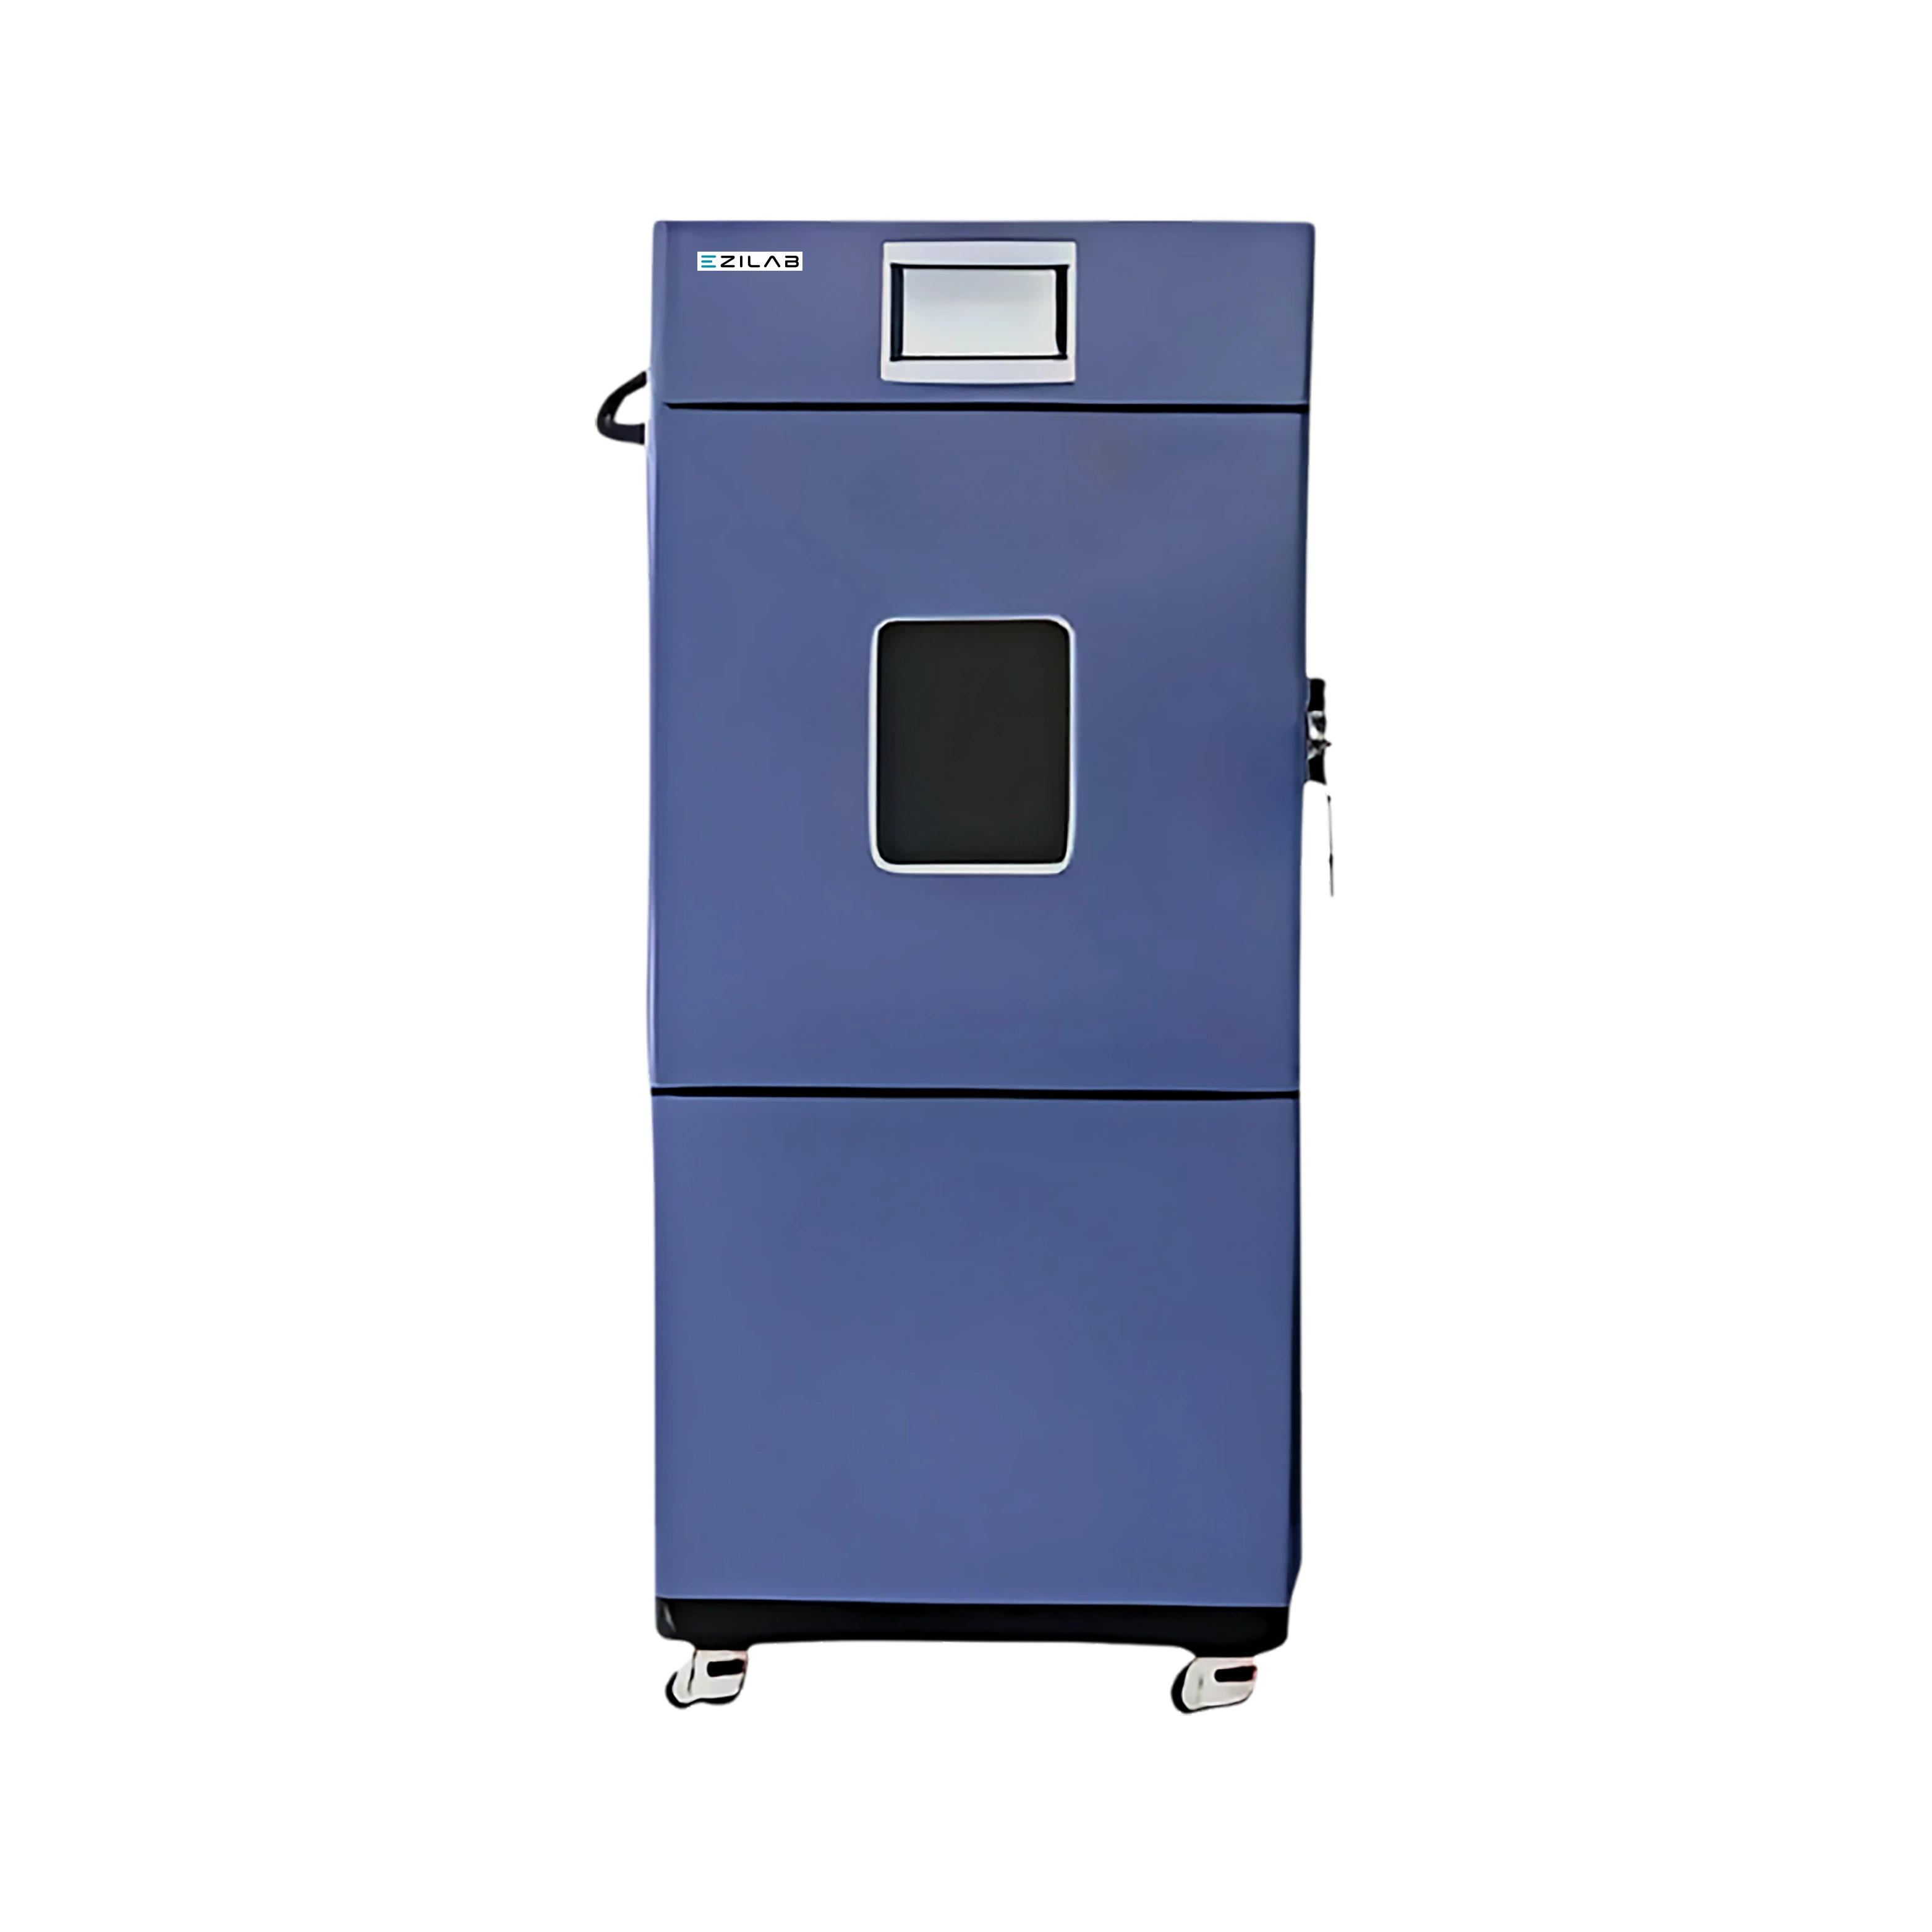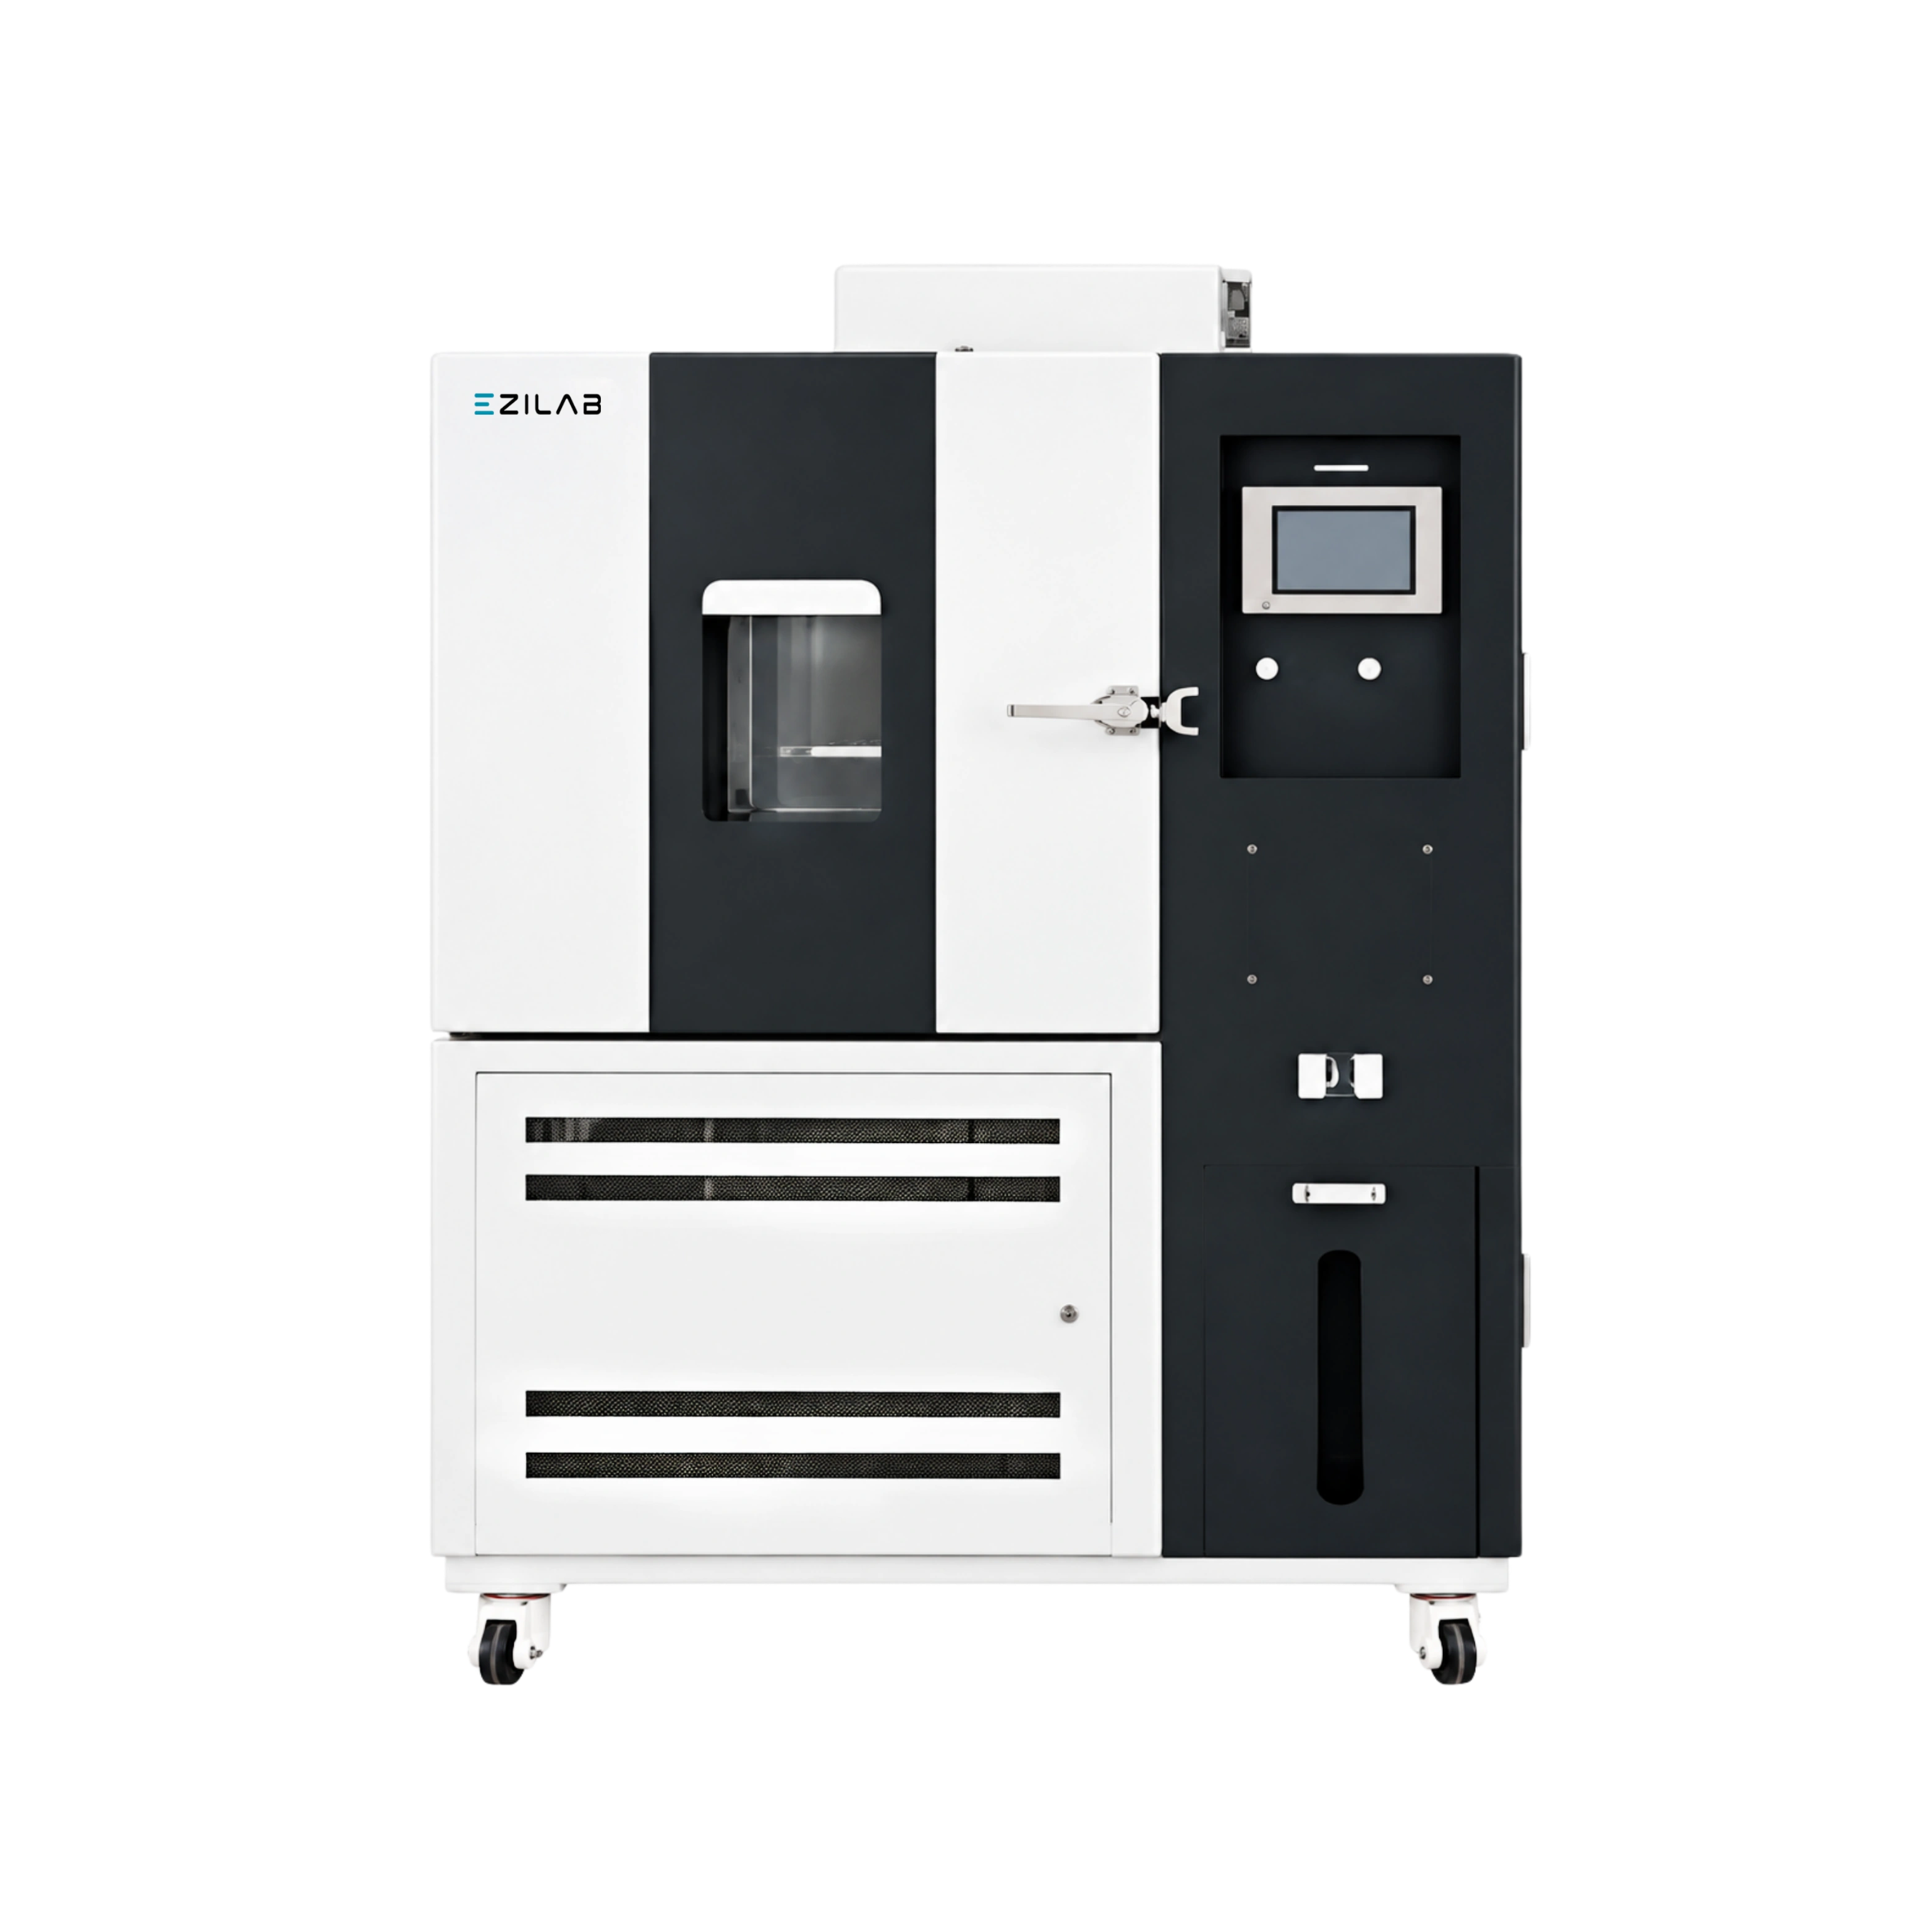
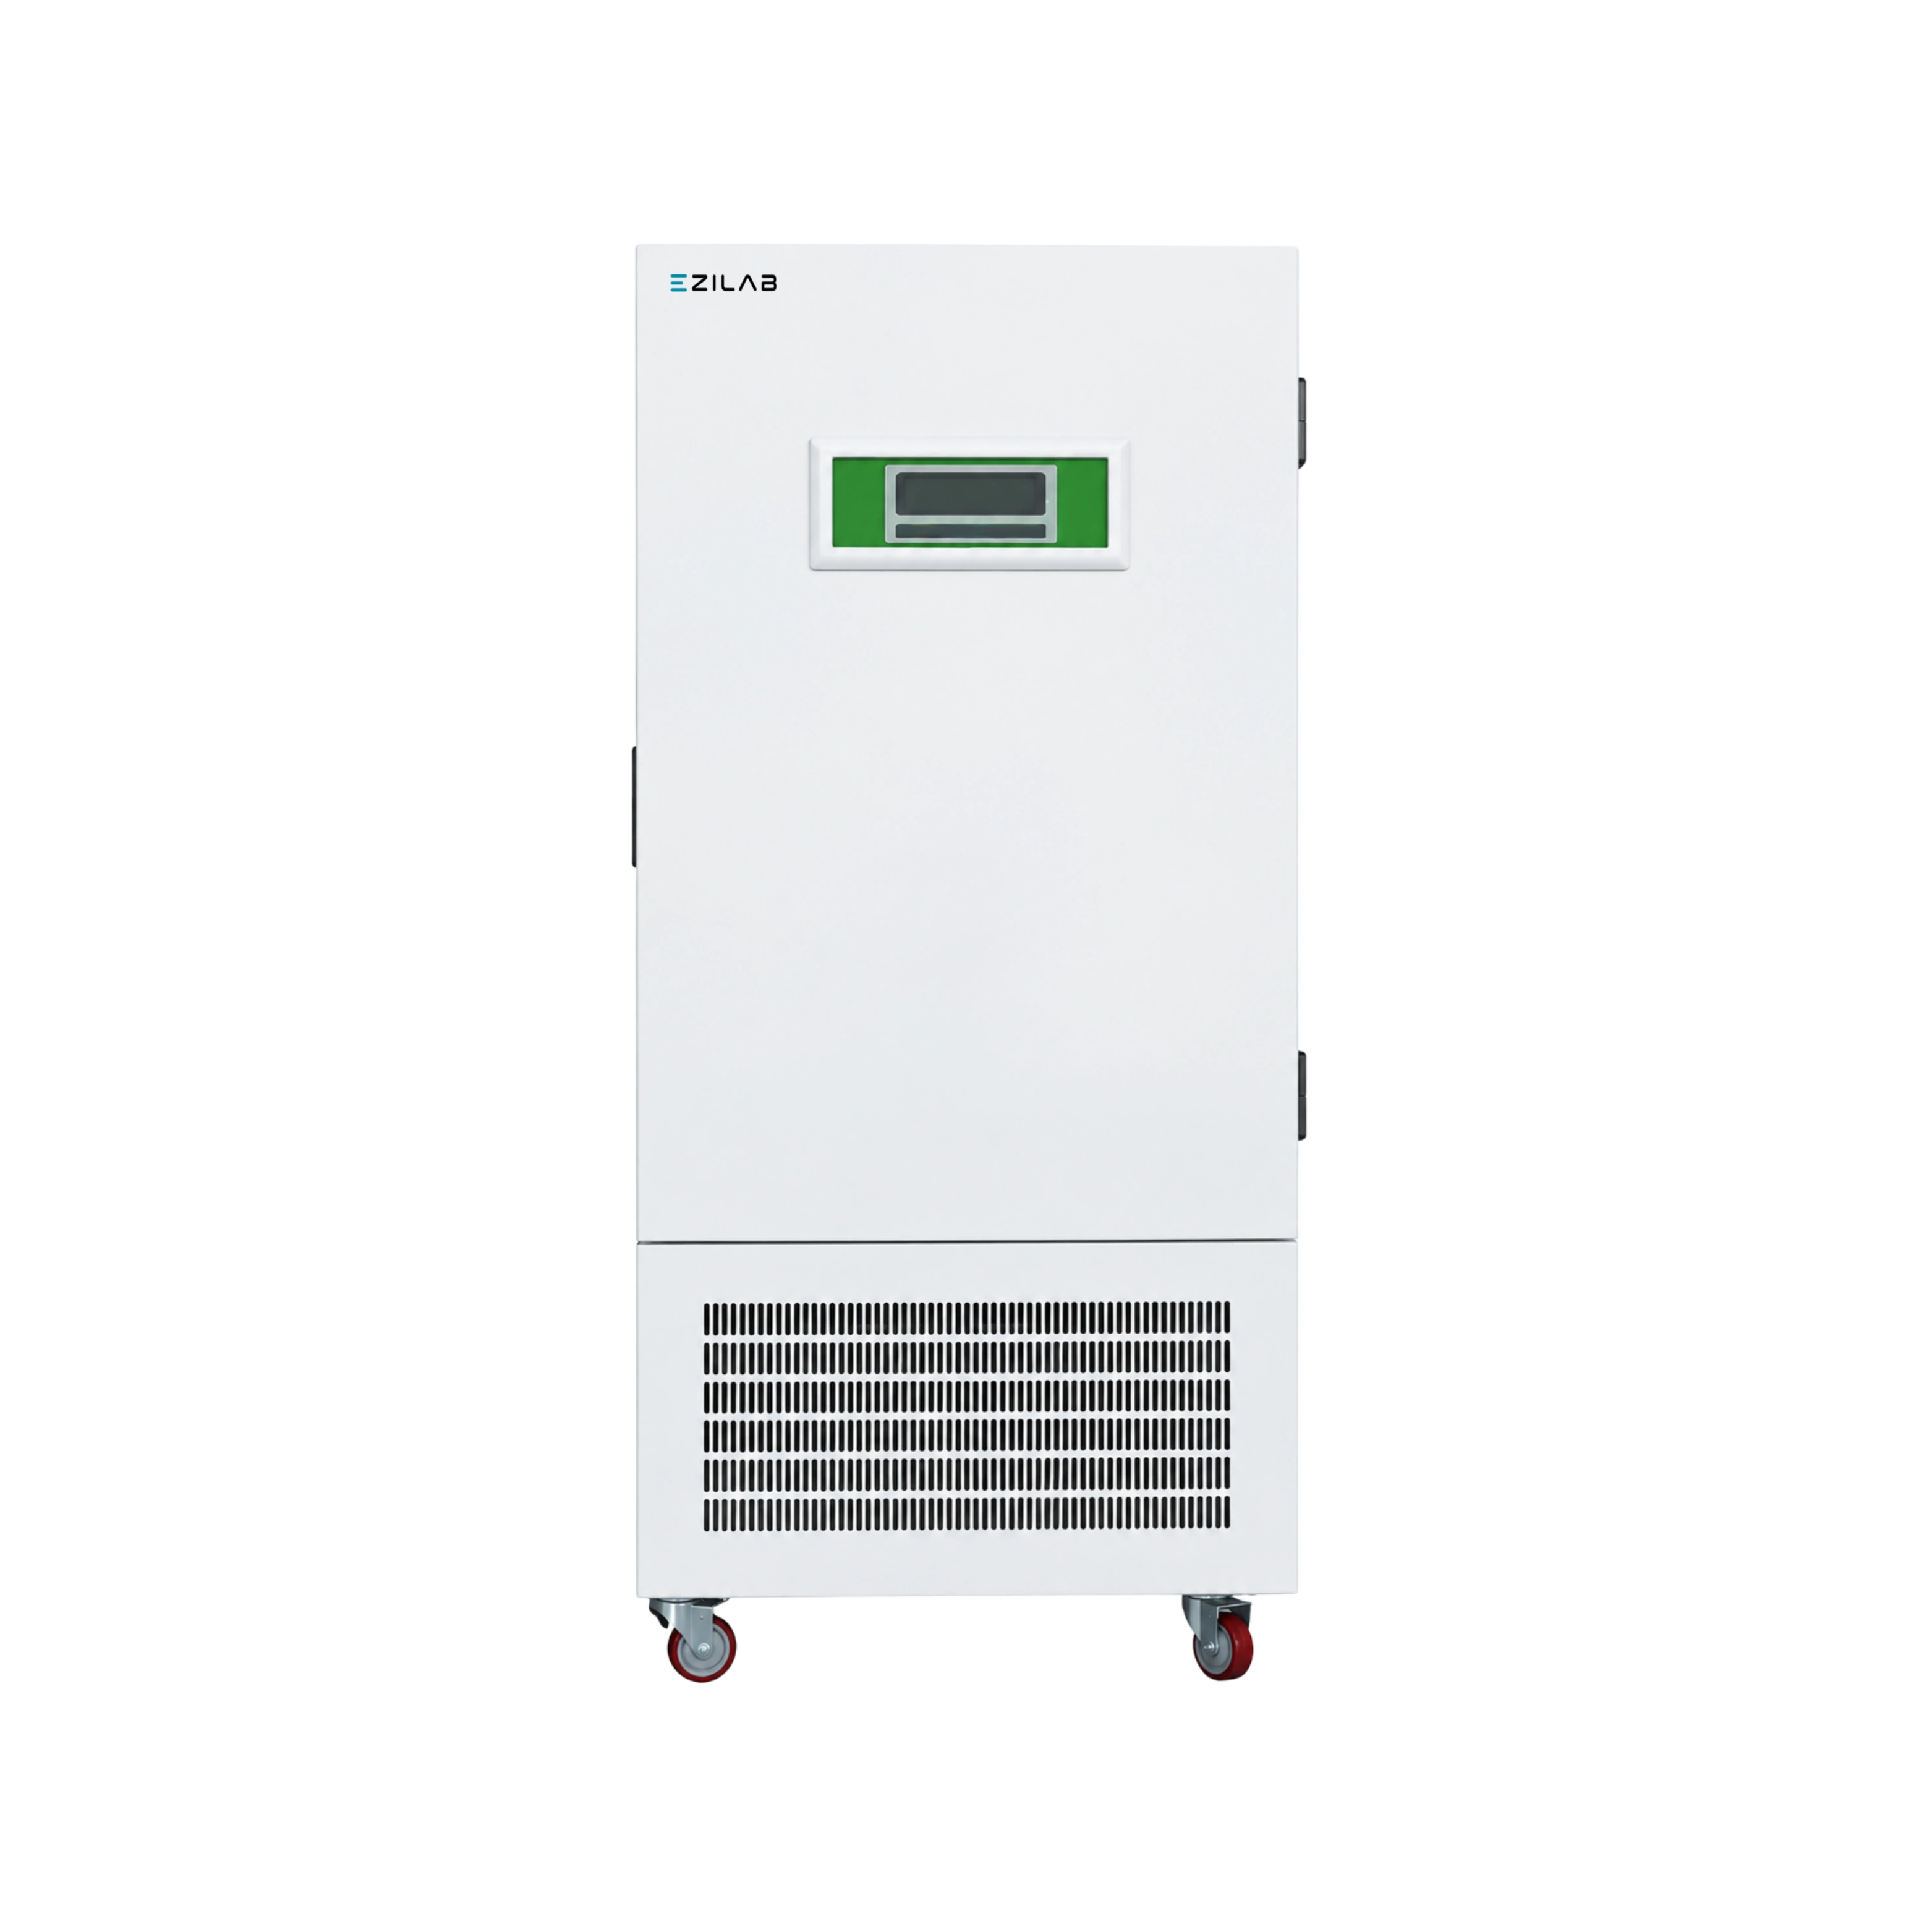
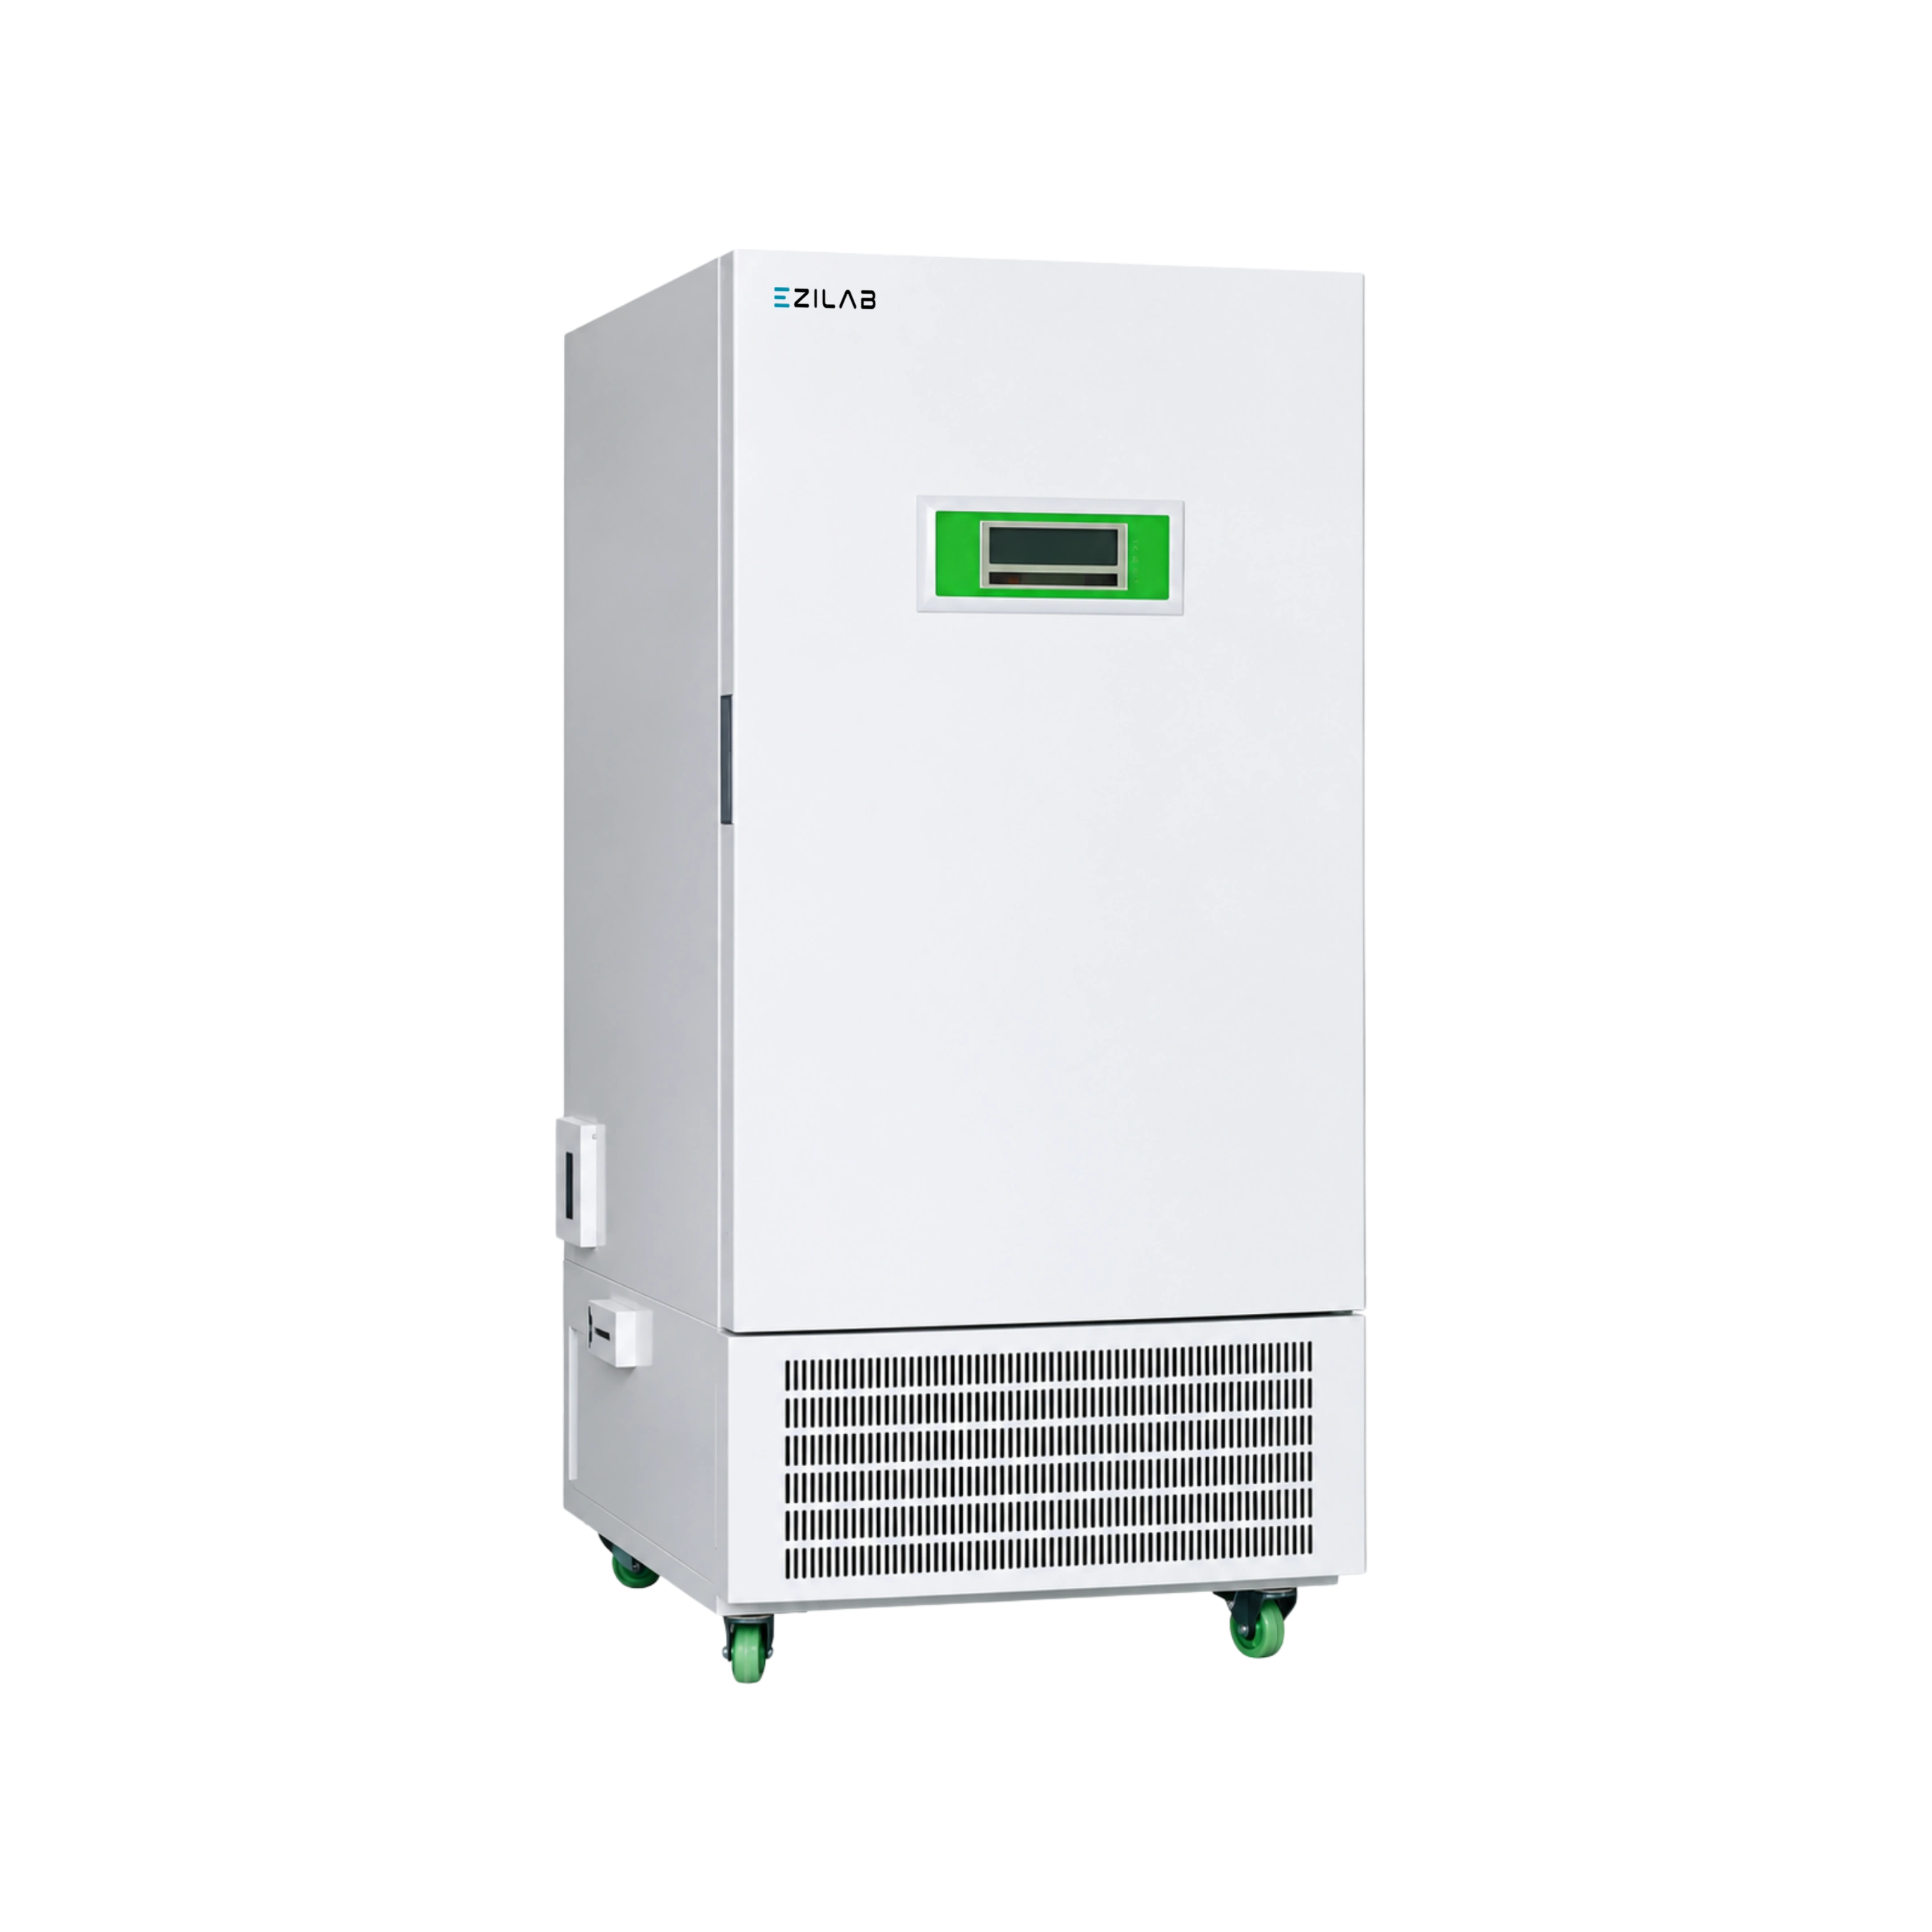
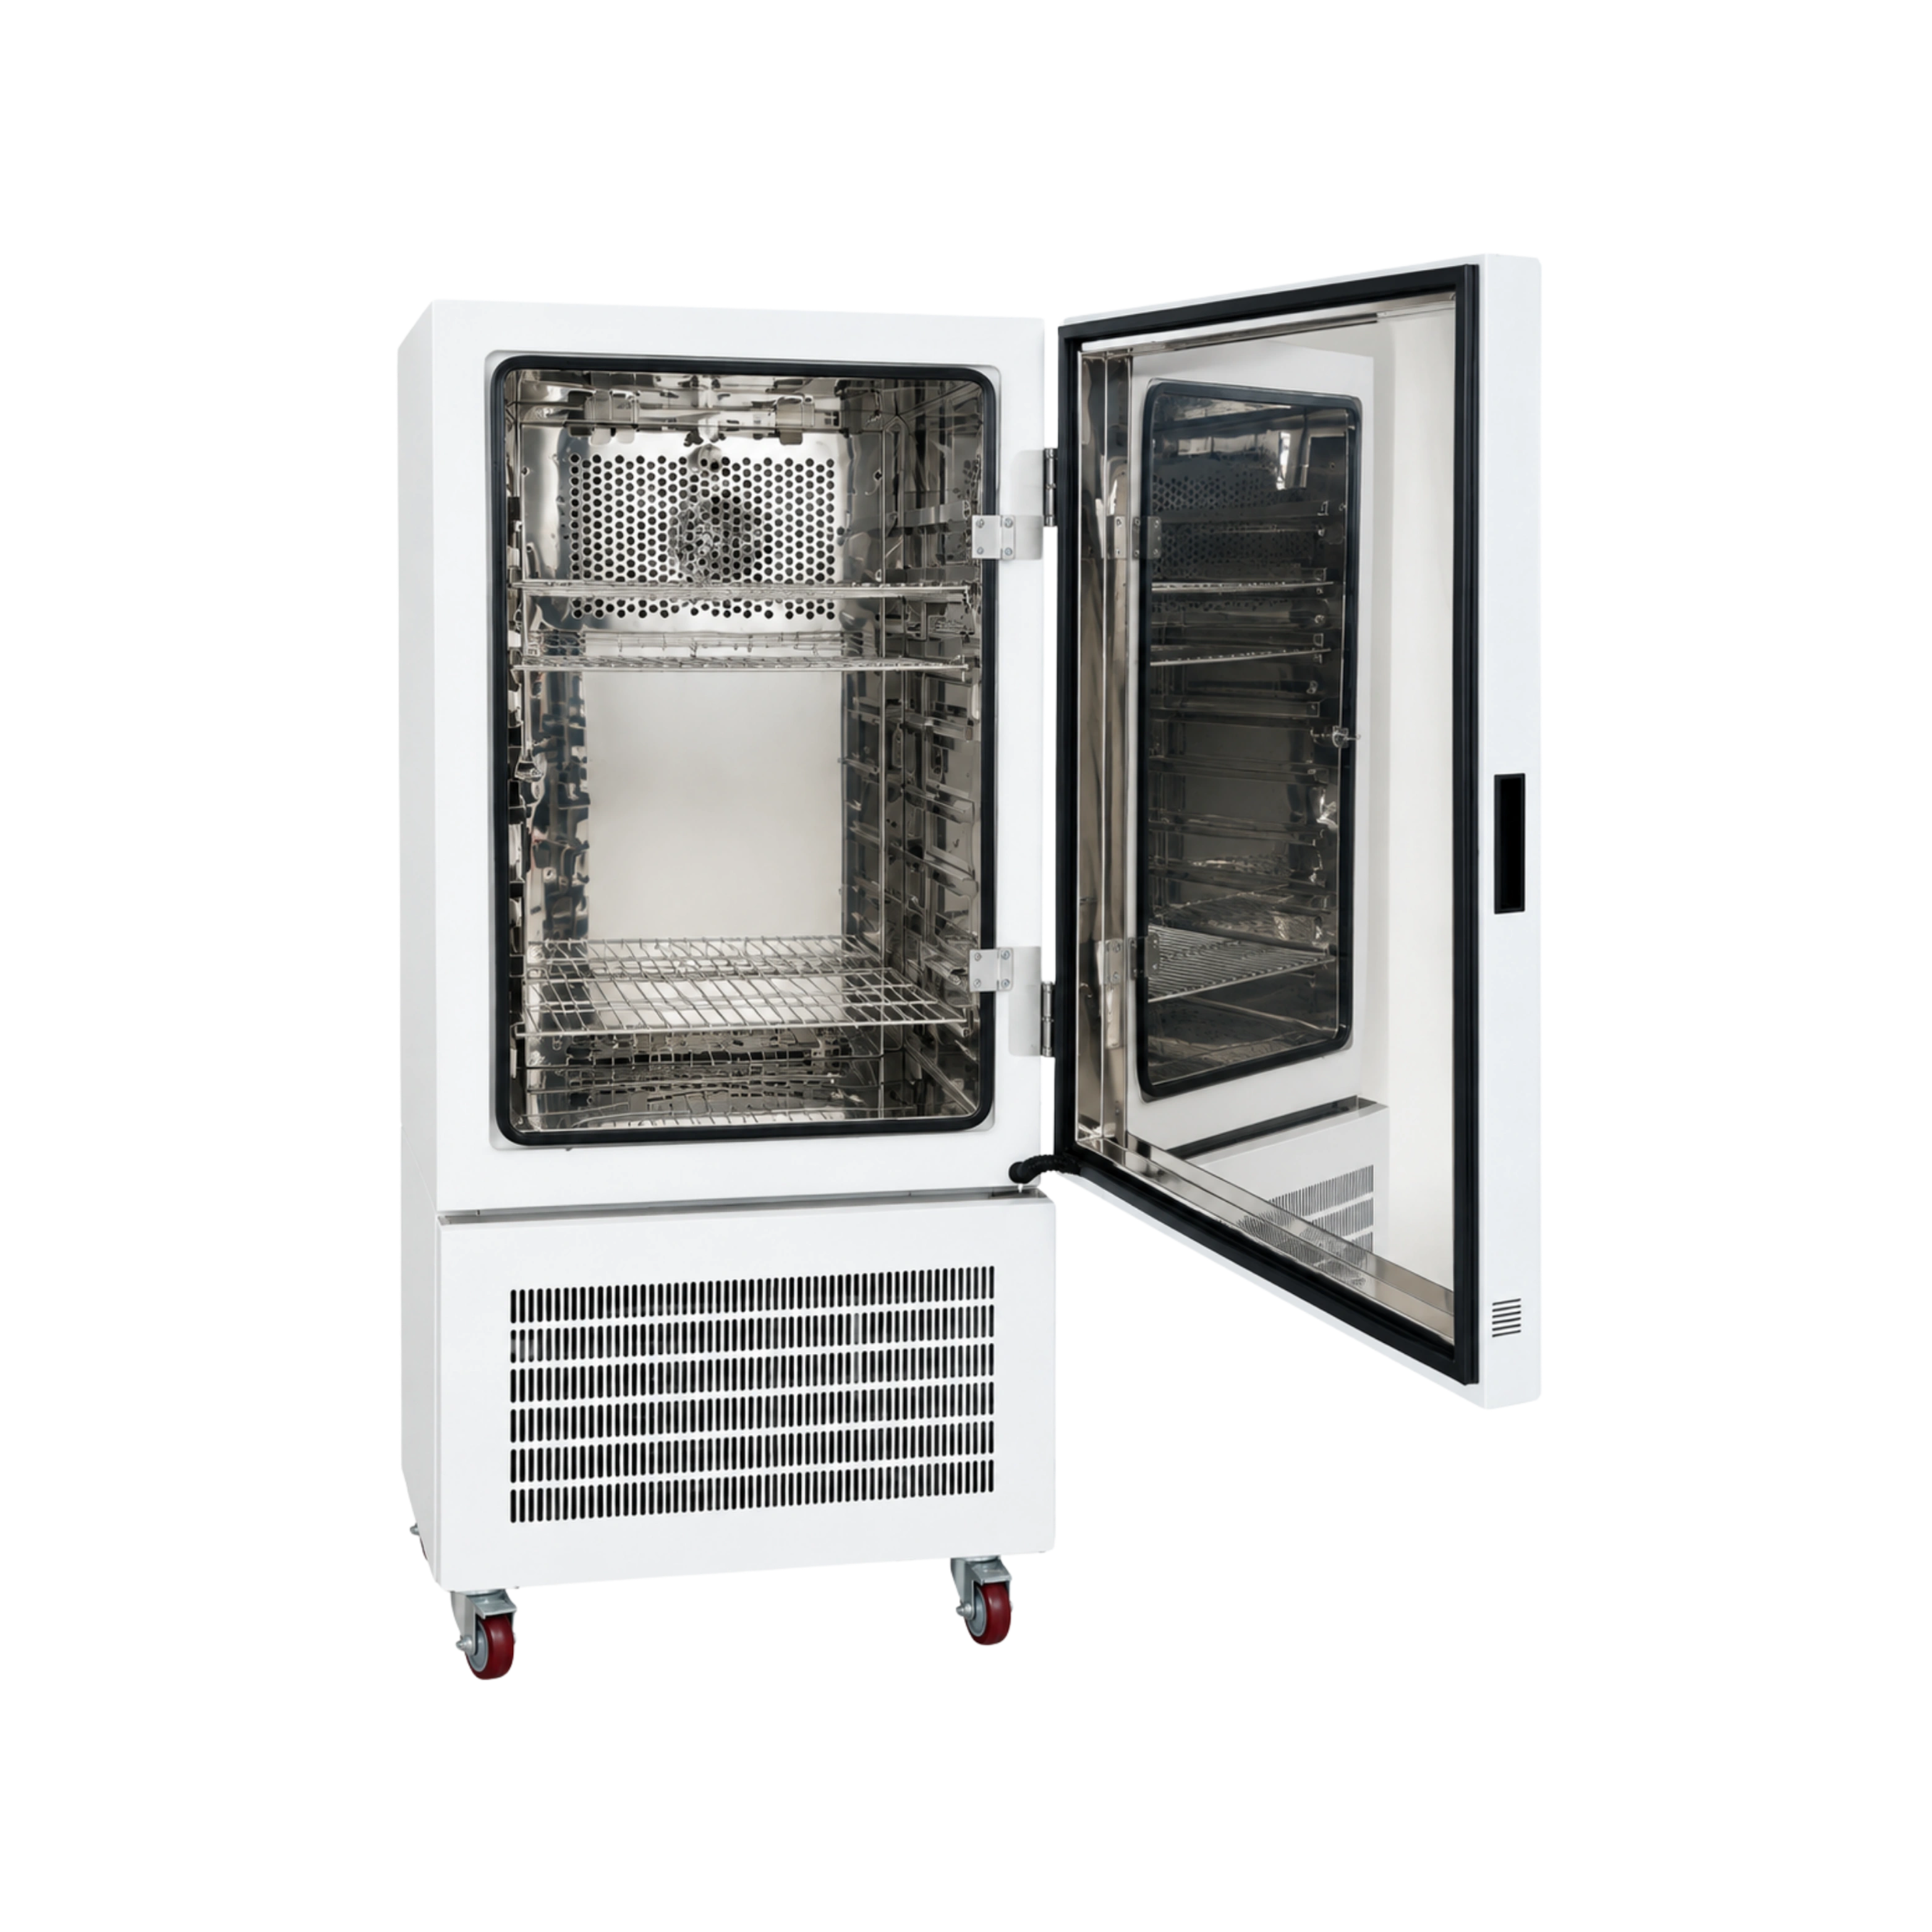
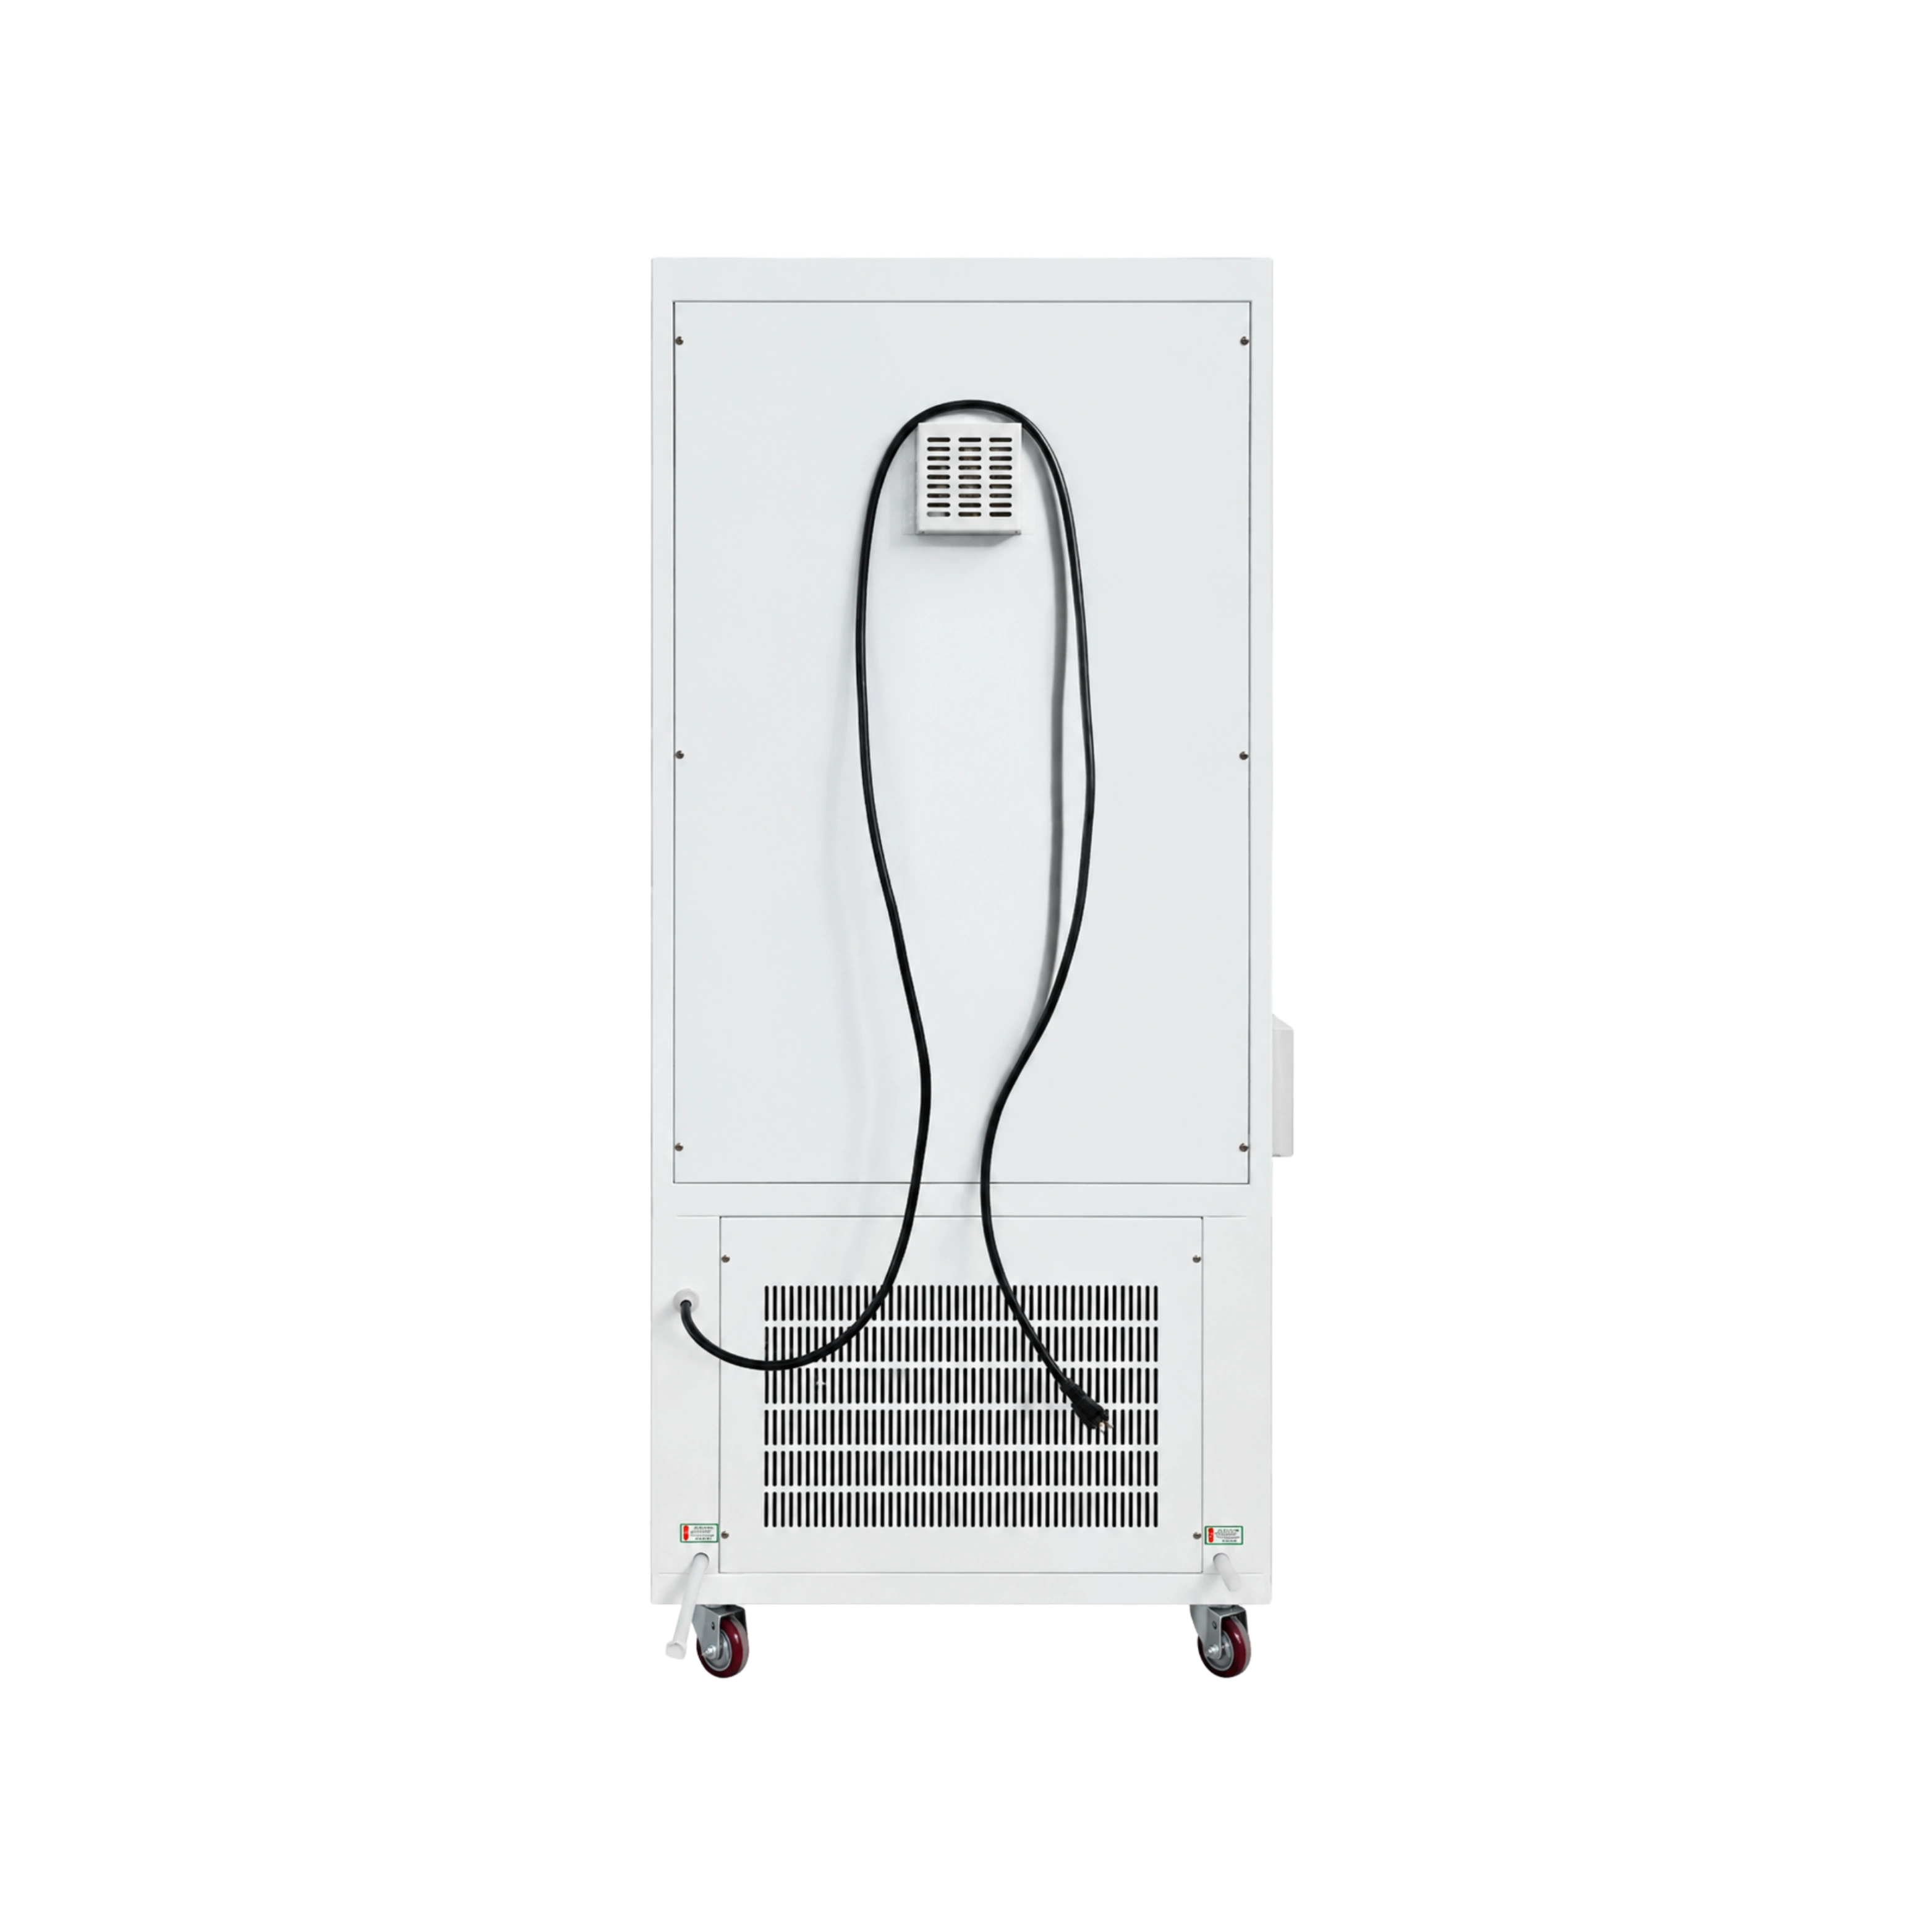
EziLab offers the Temperature and Humidity Test Chamber EZL-TH165, a large stability chamber with 800 L volume for full production batch testing and multi-product environmental studies. Its 965 × 610 × 1370 mm interior offers more space than standard units, so multiple sample sets run under identical conditions. Temperature adjusts from 0 to 65°C with ±1°C uniformity, ±0.5°C fluctuation at high temperatures, and ±1°C at low temperatures, while humidity control spans 40% to 90% RH with ±3% RH fluctuation. An R134a refrigeration system and 4000 W power rating maintain stable conditions over long test cycles. Movable stainless steel grids adjust to sample size, and durable stainless steel construction resists corrosion in humid environments. Over temperature protection and leakage protection safeguard samples and users, and a user-friendly interface simplifies programming. In industrial settings, pharmaceutical manufacturers use this climate test chamber for drug stability studies, shelf-life evaluation, and packaging performance checks. Food and beverage producers run quality control tests on product shelf stability and moisture sensitivity, while industrial laboratories examine how materials respond to heat and humidity. Research units use it for controlled experiments. Measuring your largest sample tray against the 965 × 610 × 1370 mm interior comes before any comparison across the Climate Test Chamber category and Temperature and Humidity Test Chamber range.
| Volume | 800 L |
|---|---|
| Temperature Range | 0 to 65˚C |
| Operation Temperature | 5 to 40 ˚C |
| Temperature Uniformity | ± 1℃ |
| Temperature Fluctuation | Low temperature ±1℃, High temperature ±0.5℃ |
| Humidity Control Range | 40% to 90%RH |
| Humidity Fluctuation | ±3 % RH |
| Refrigerant | R134a |
| Power Rating | 4000W |
| Chamber Size (W × D × H ) | 965 × 610 × 1370 mm |
| Exterior Size (W × D × H ) | 110 x 930 x 2270 mm |
Movable stainless grid
Over temperature protection
Leakage protection
Durable stainless steel
User friendly interface
| • | Used by pharmaceutical manufacturers for drug stability studies and shelf-life evaluation. |
| • | Applied in packaging performance checks for pharmaceutical products. |
| • | Employed by food and beverage producers for quality control tests on shelf stability and moisture sensitivity. |
| • | Suited to industrial laboratories examining how materials respond to heat and humidity. |
| • | Supports scientific research units in controlled experiments. |
| • | Handles full production batch testing and multi-product environmental studies in a large chamber. |